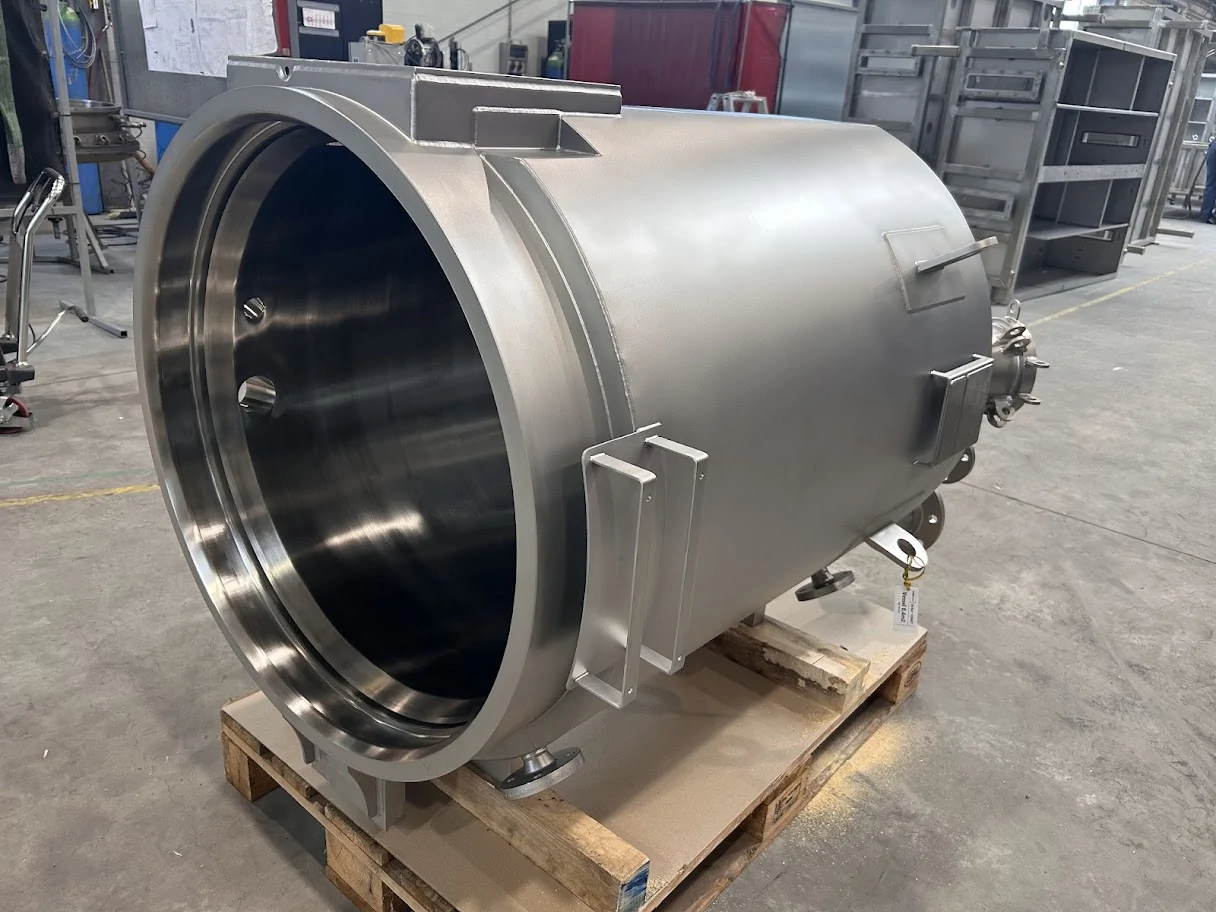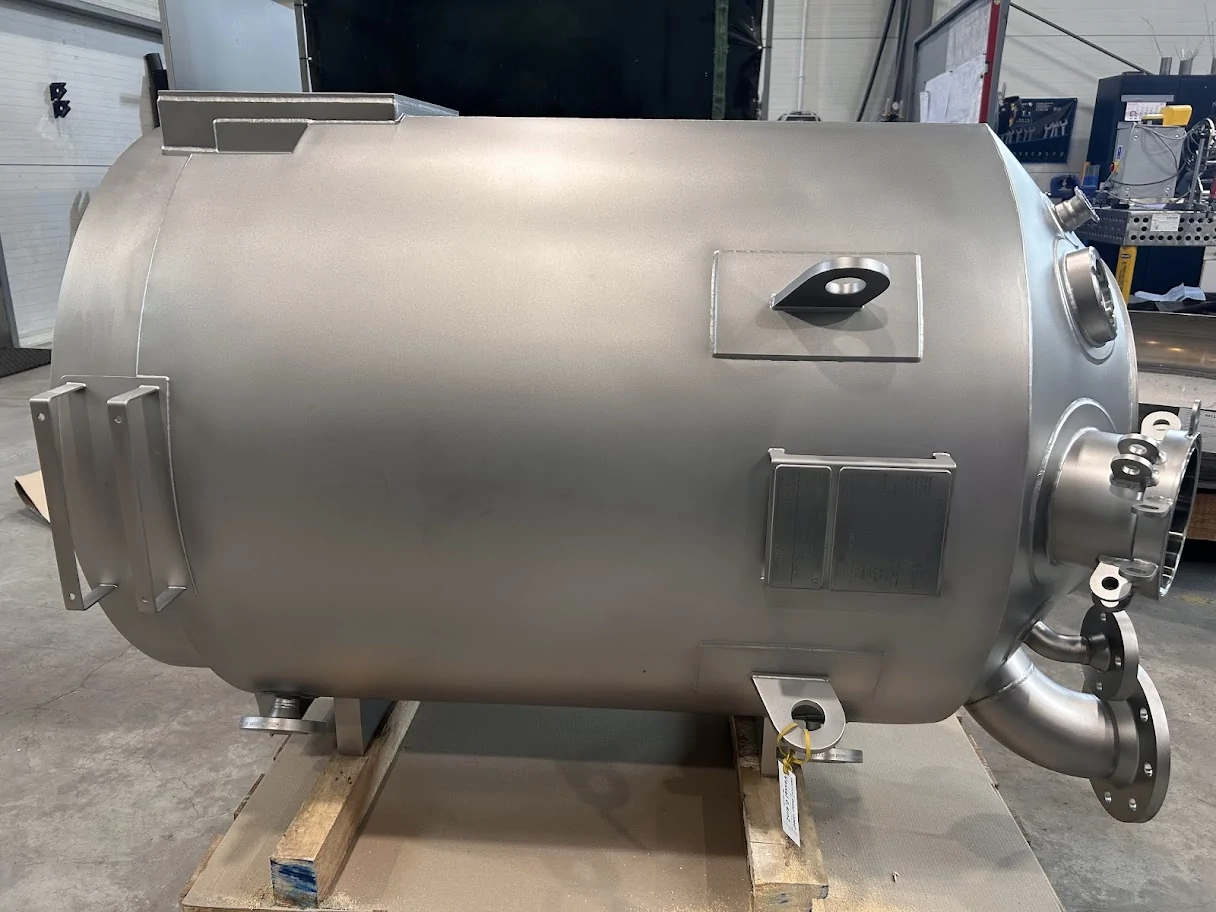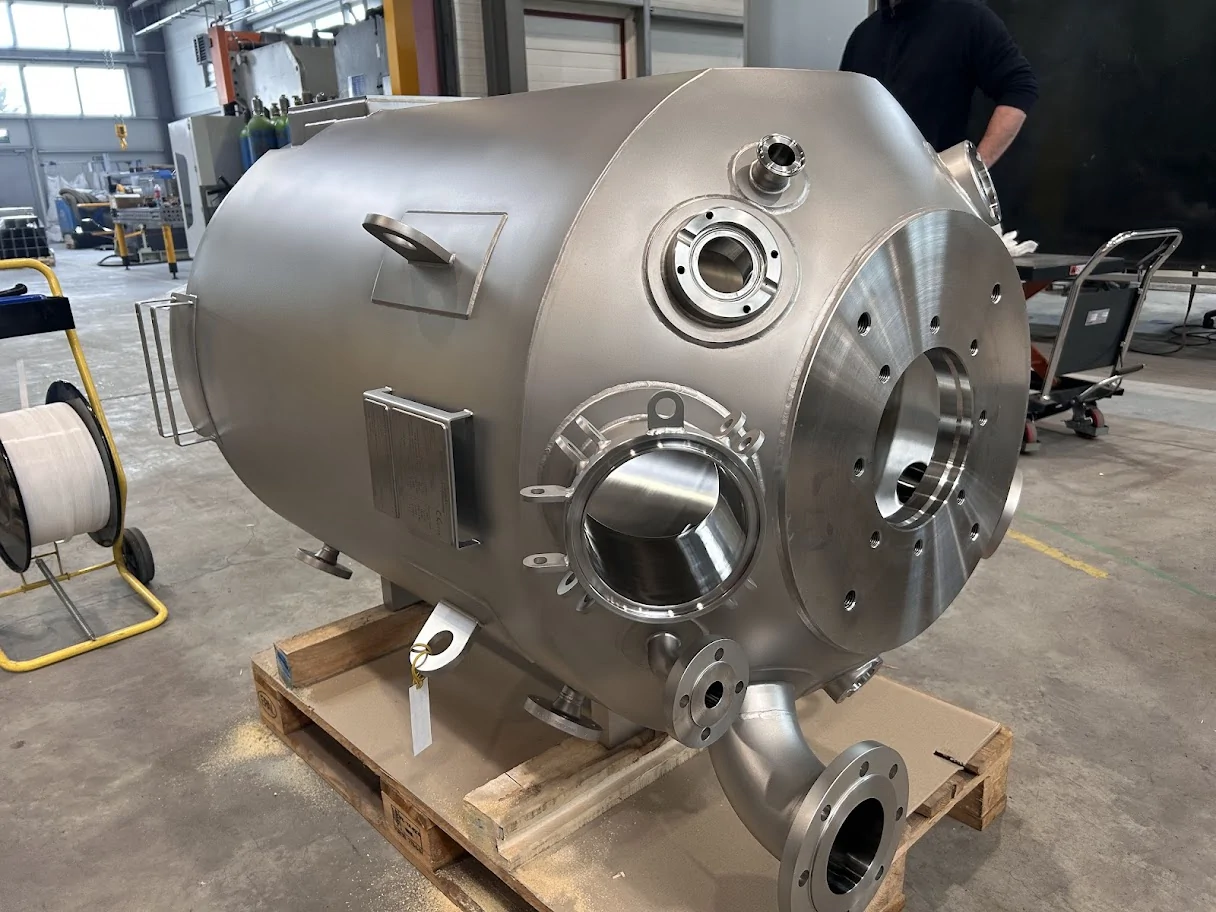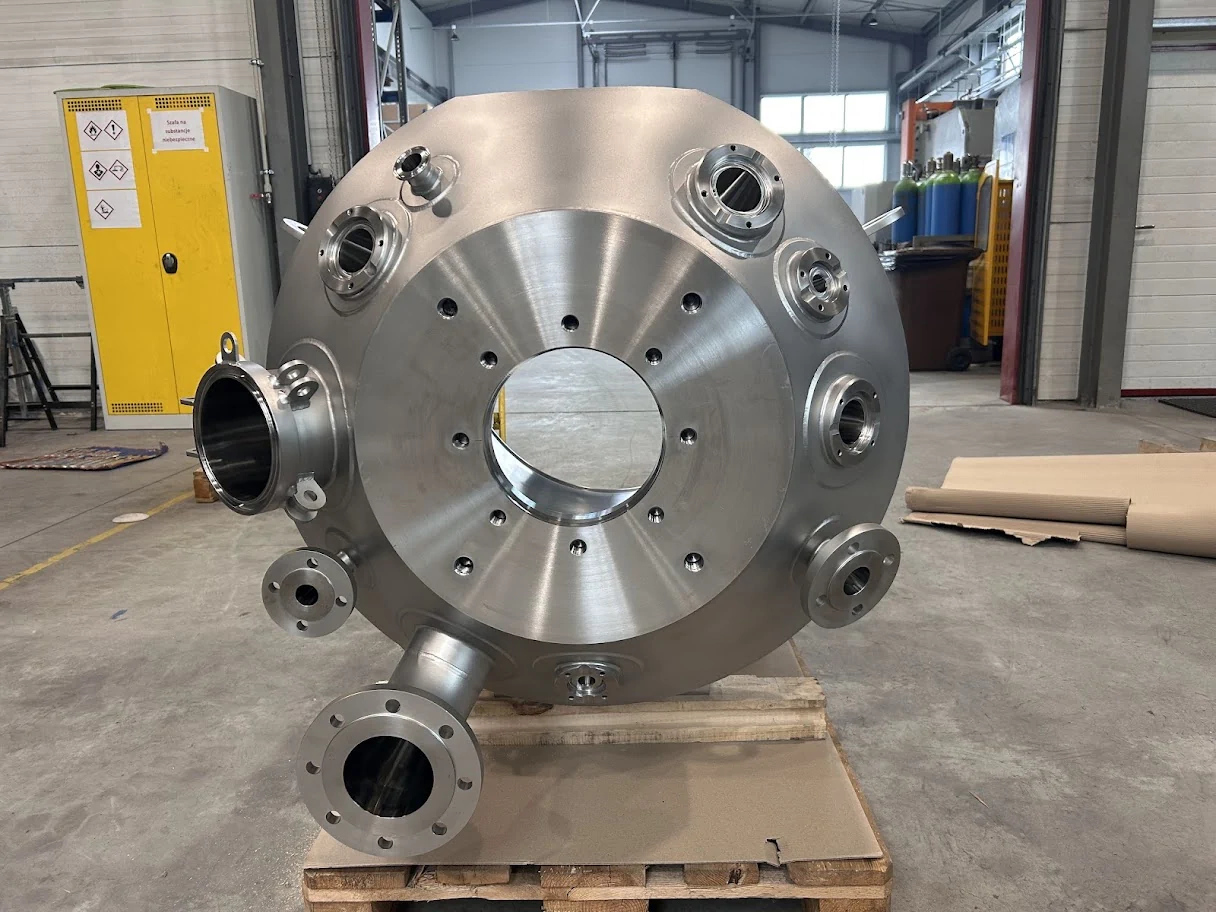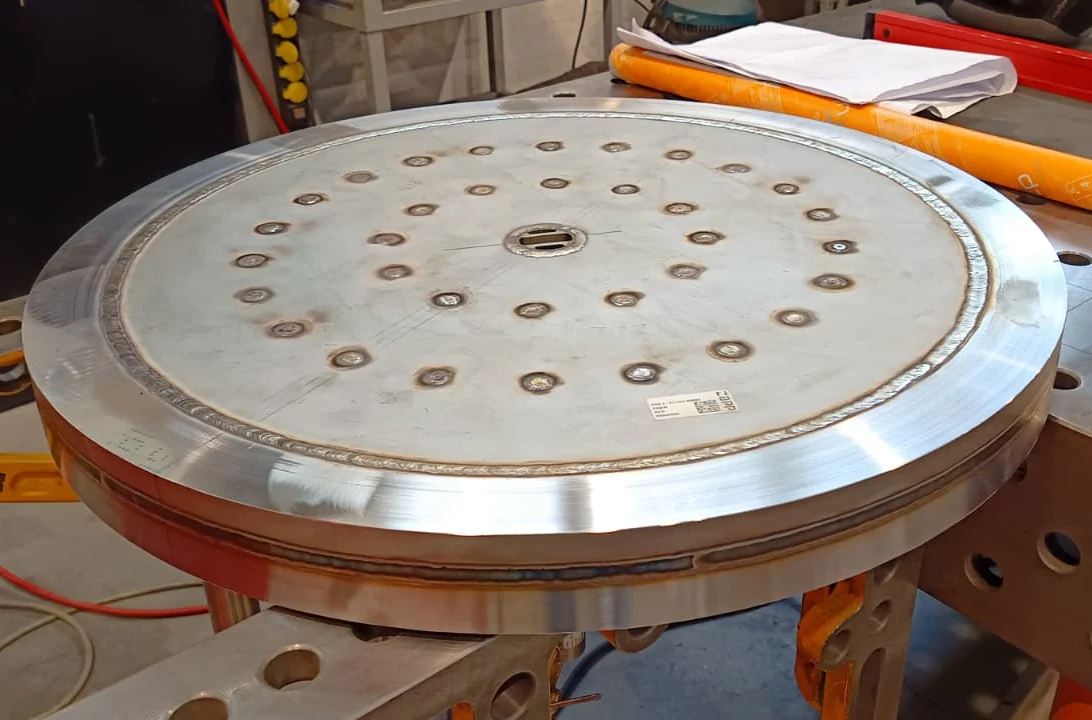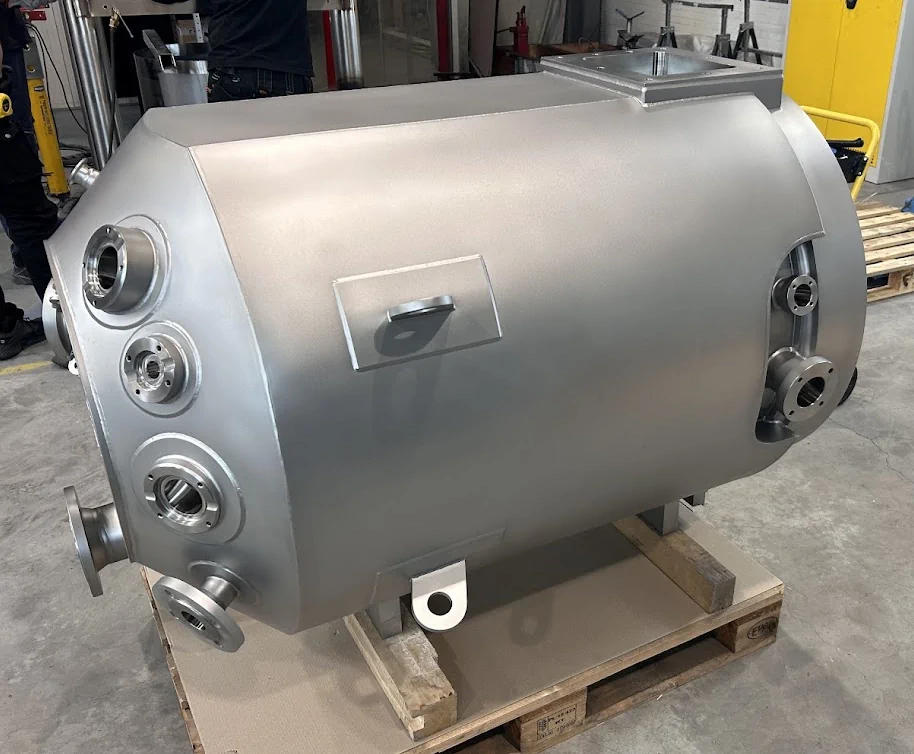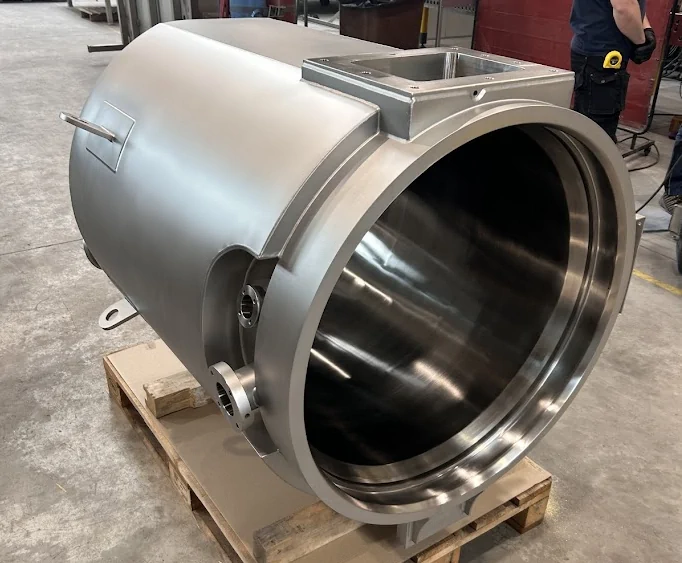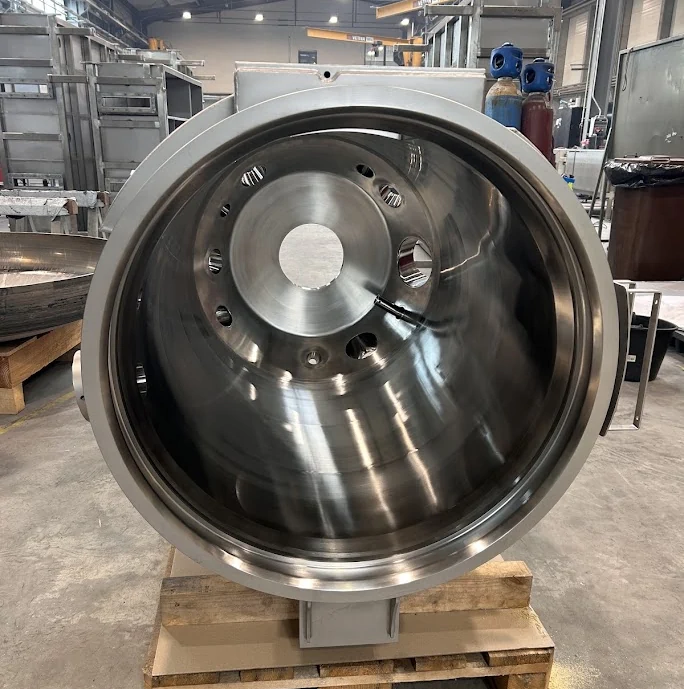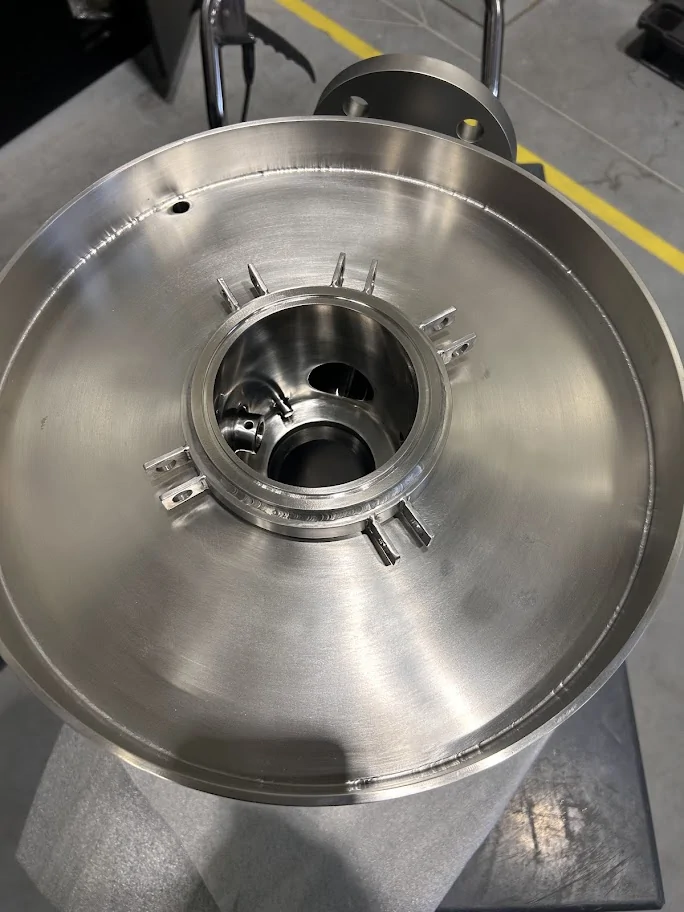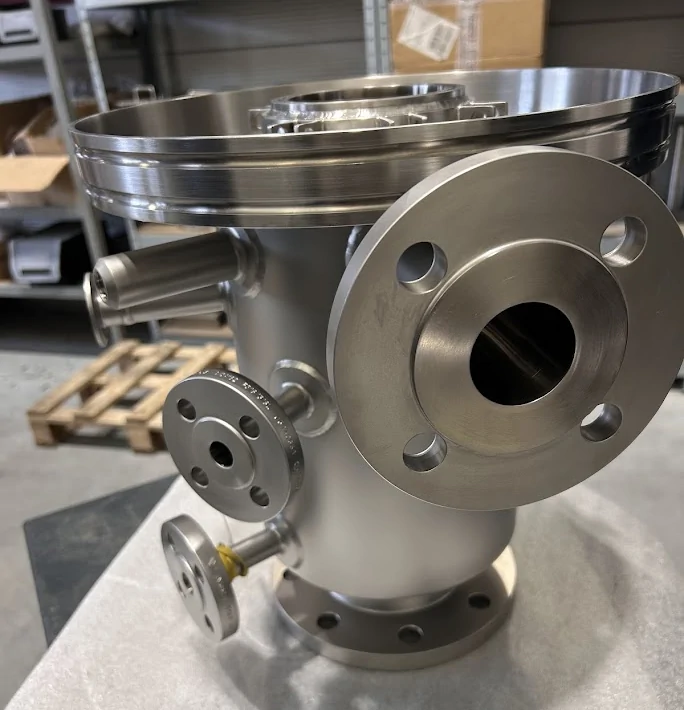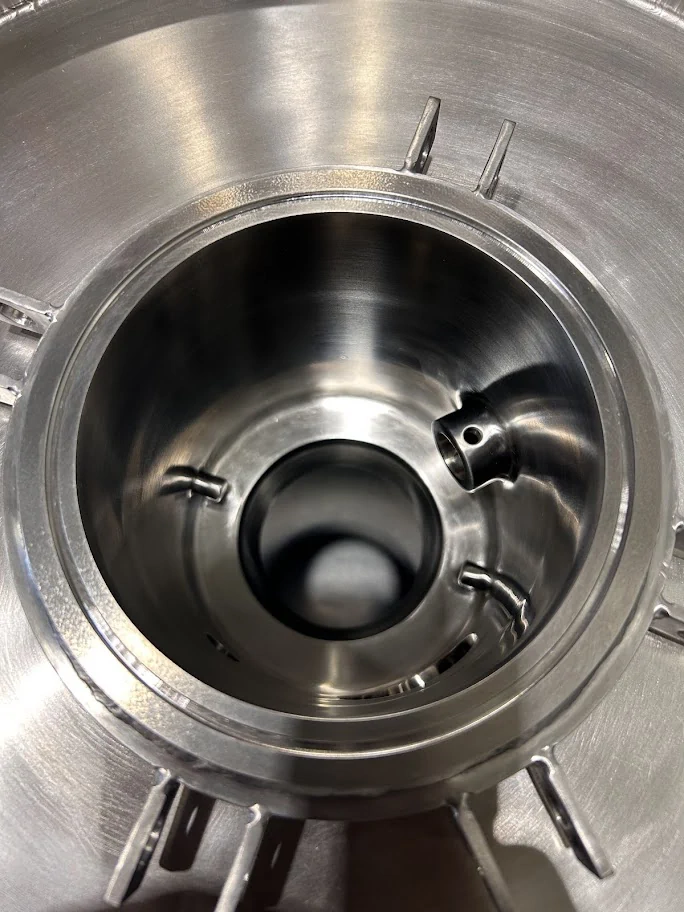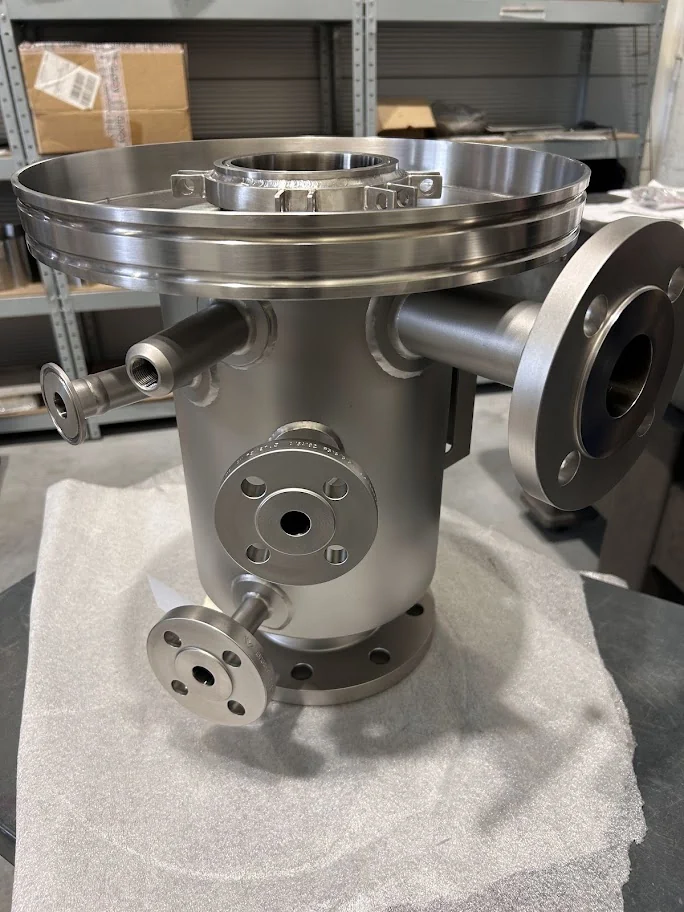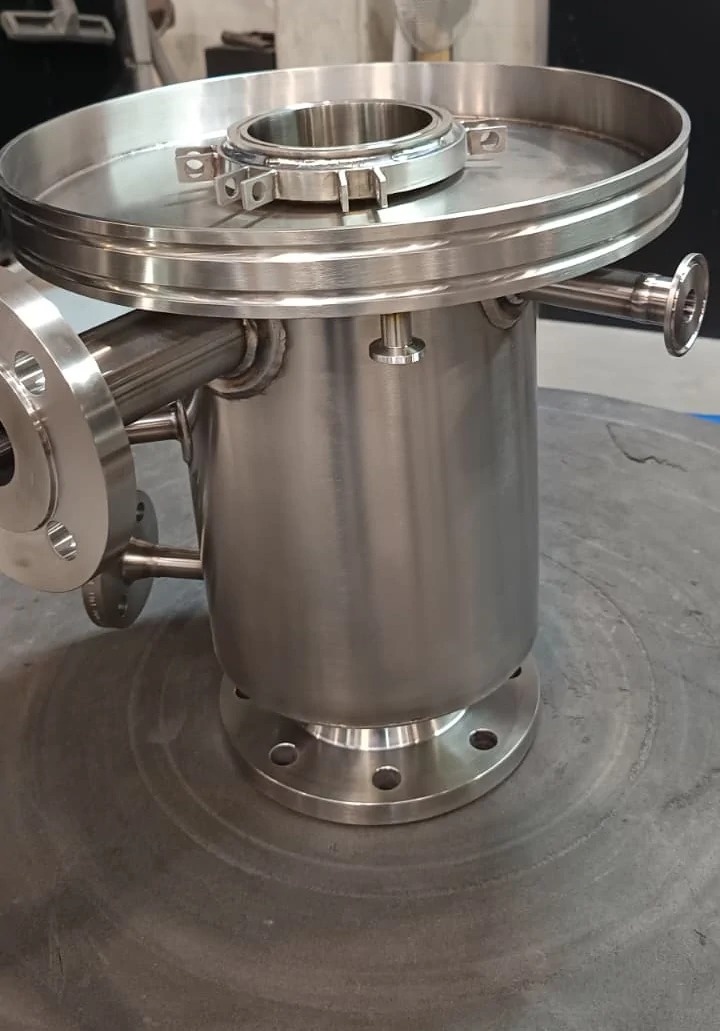
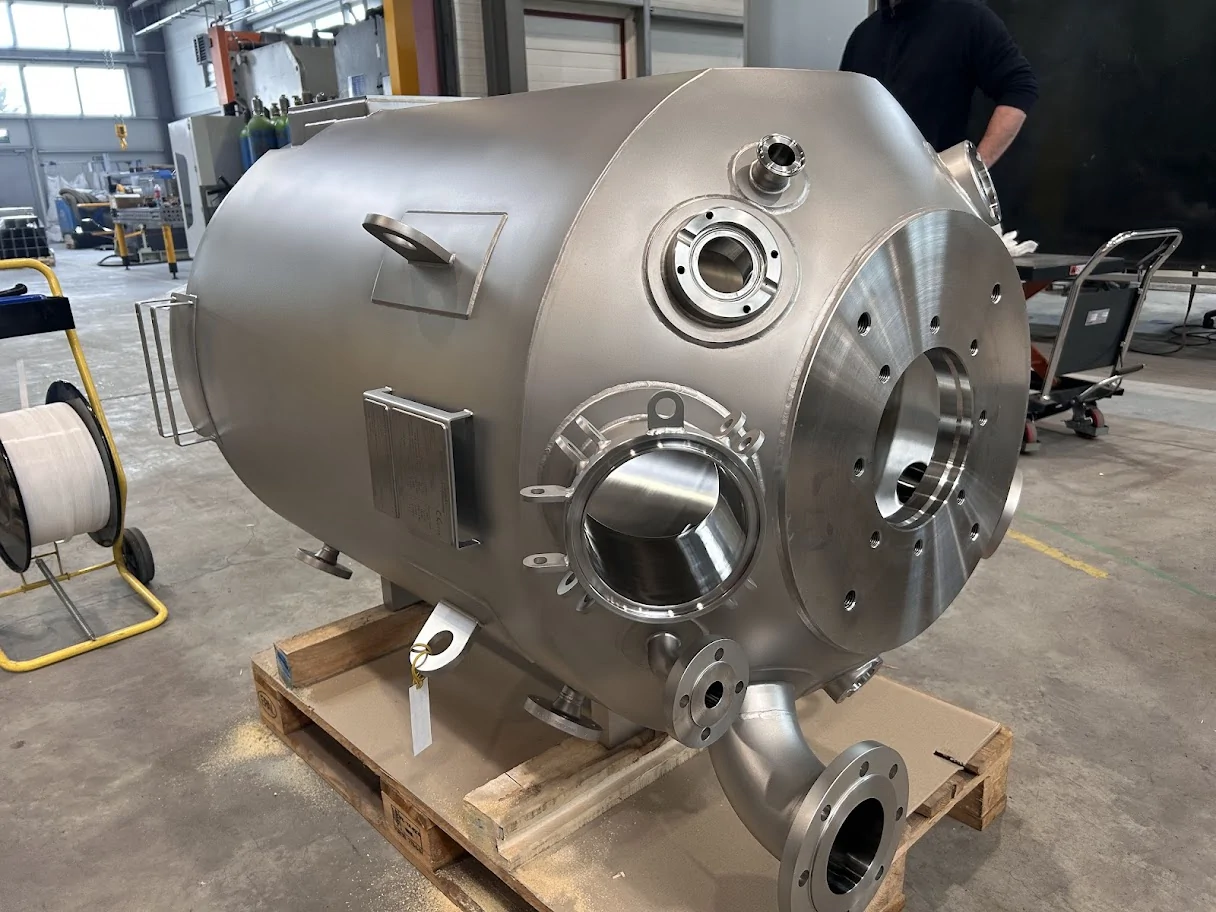
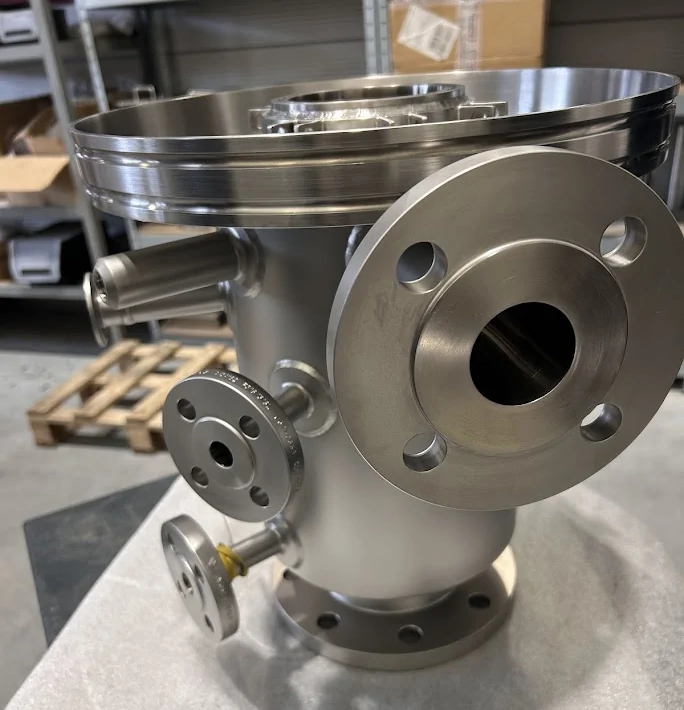
As part of this project, we manufactured a specialized filter drier engineered to operate in a demanding process environment. Components coming into direct contact with the product were fabricated from Hastelloy C22 / 2.4602, while non-contact structural elements were made of 316L / 1.4404 stainless steel.
A critical milestone of the project involved the final machining of the sealing surfaces. In the most sensitive areas, the required manufacturing tolerance was ±0.1 mm, demanding exceptional precision, technical expertise, and rigorous quality control at every stage of production.
Category
Number of hours worked
2,160 h
Internal surface roughness
Ra 0.5
Dimensions
Diameter 724 mm,
height 1,350 mm
Project assumptions
The main assumption of the project was to manufacture a specialized filter dryer using materials tailored to the process requirements and operating conditions of the equipment. Parts in contact with the product were made of Hastelloy C22 / 2.4602, while elements without direct product contact were built from 316L / 1.4404 stainless steel. Maintaining the required surface quality was also essential — Ra 0.5 inside the device, alongside an external glass-beaded finish.
The second key assumption was extremely high precision in manufacturing, particularly regarding the final mechanical machining of sealing surfaces. In the most critical points, the error tolerance was only ±0.1 mm, which required strict quality control and extensive team experience. The project was executed in accordance with AD 2000-Merkblatt requirements, and its implementation involved a total of 2,160 hours of work by designers, technologists, and welders.
Technical specification
Implementation gallery