Project description
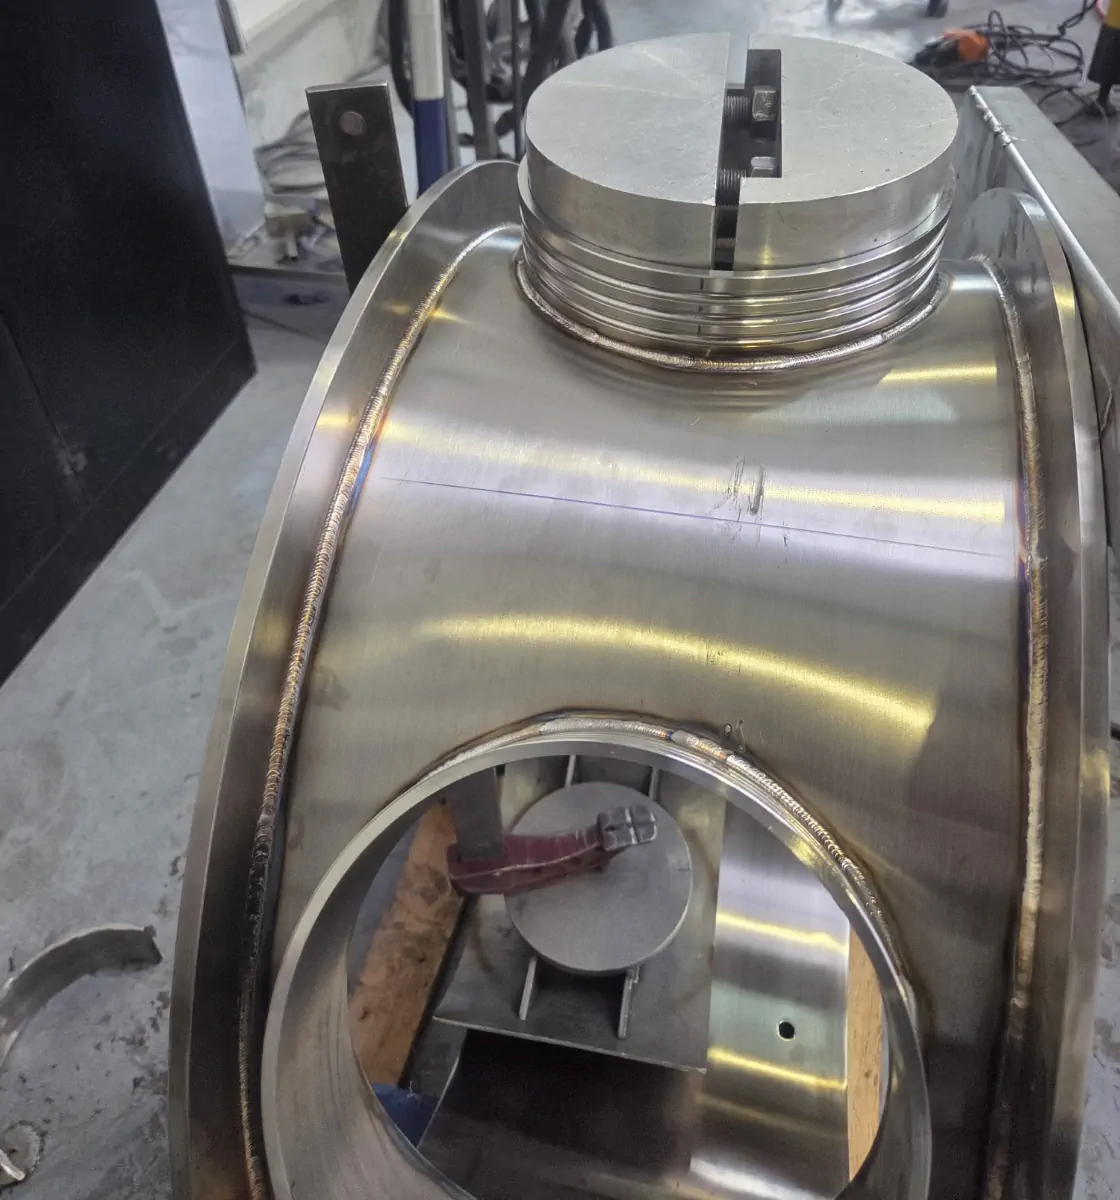
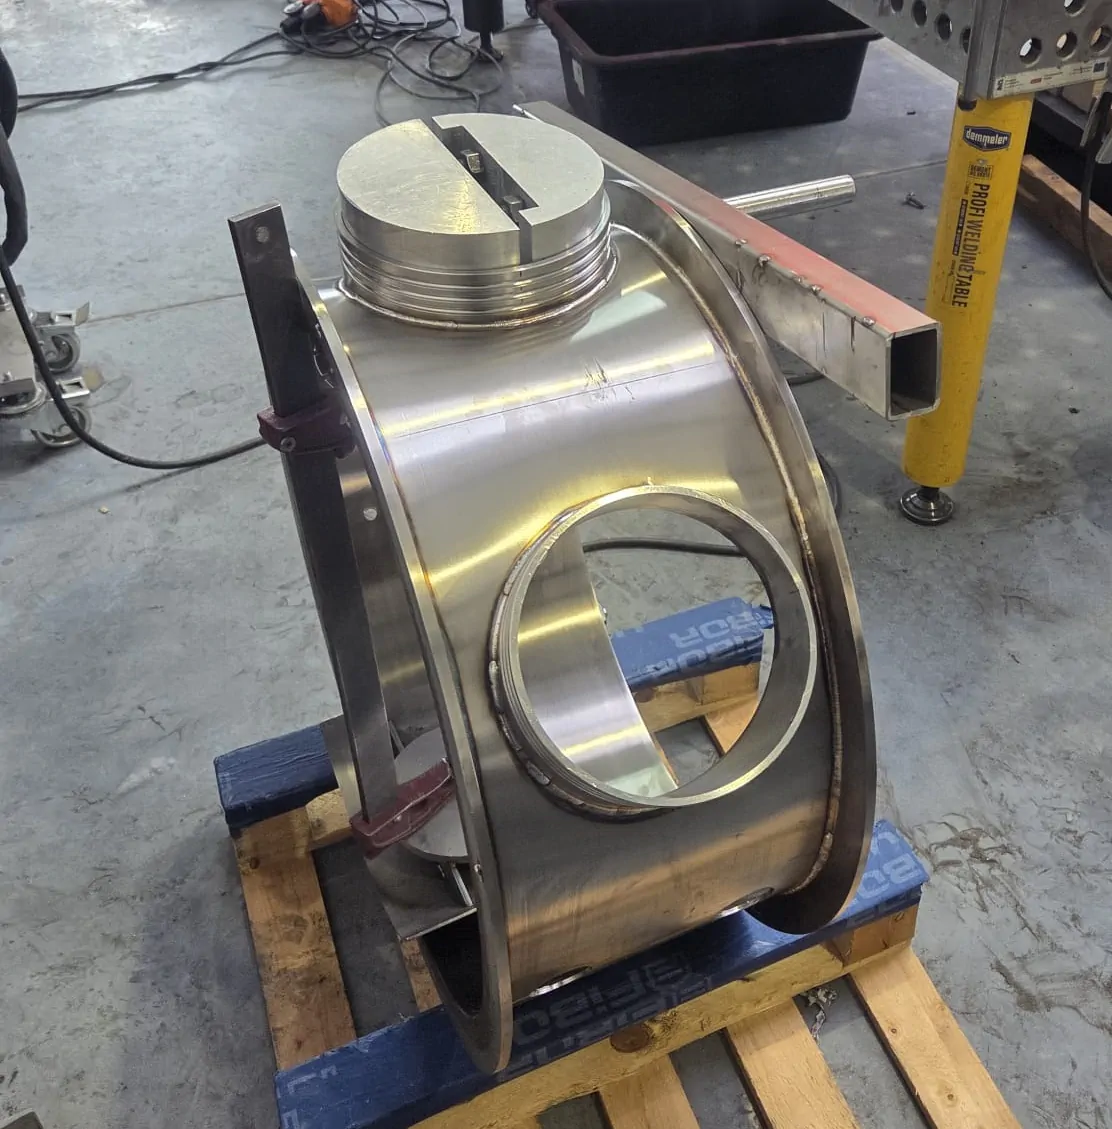
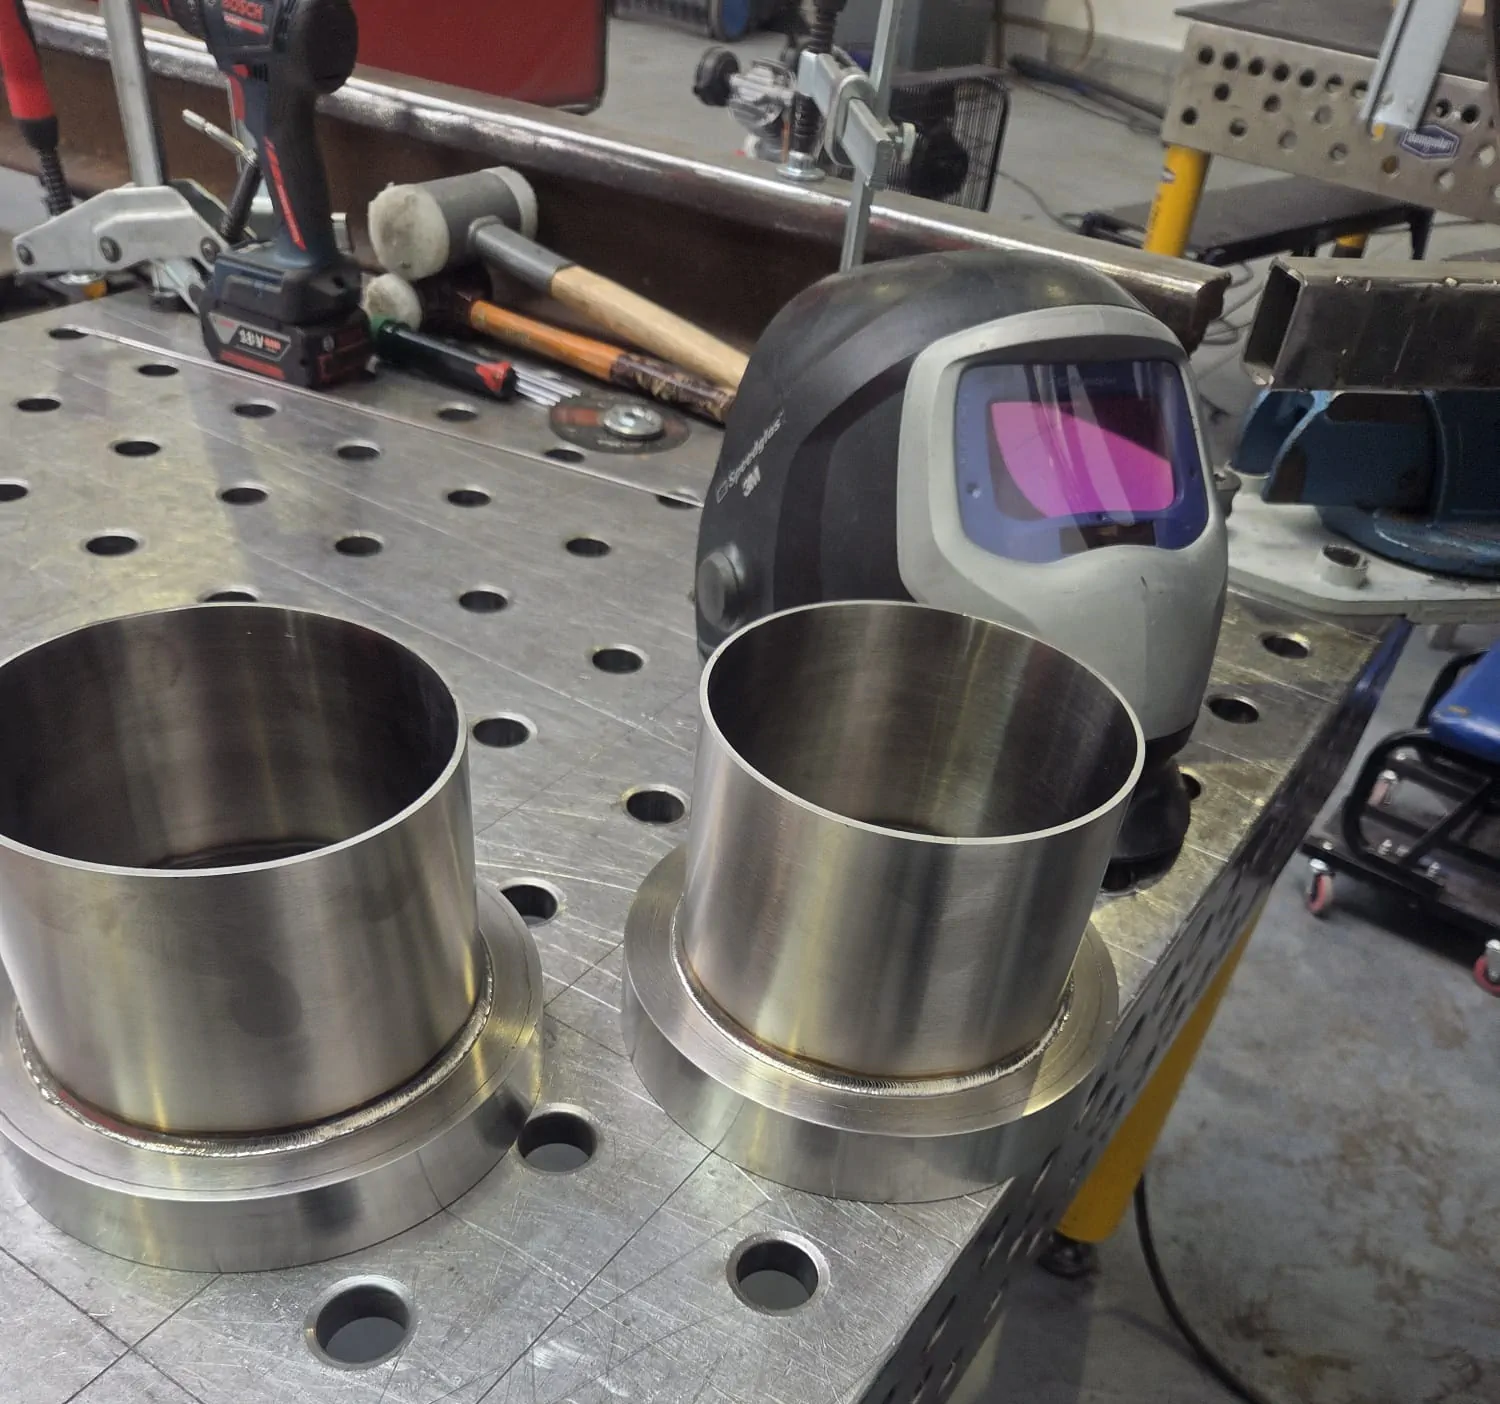
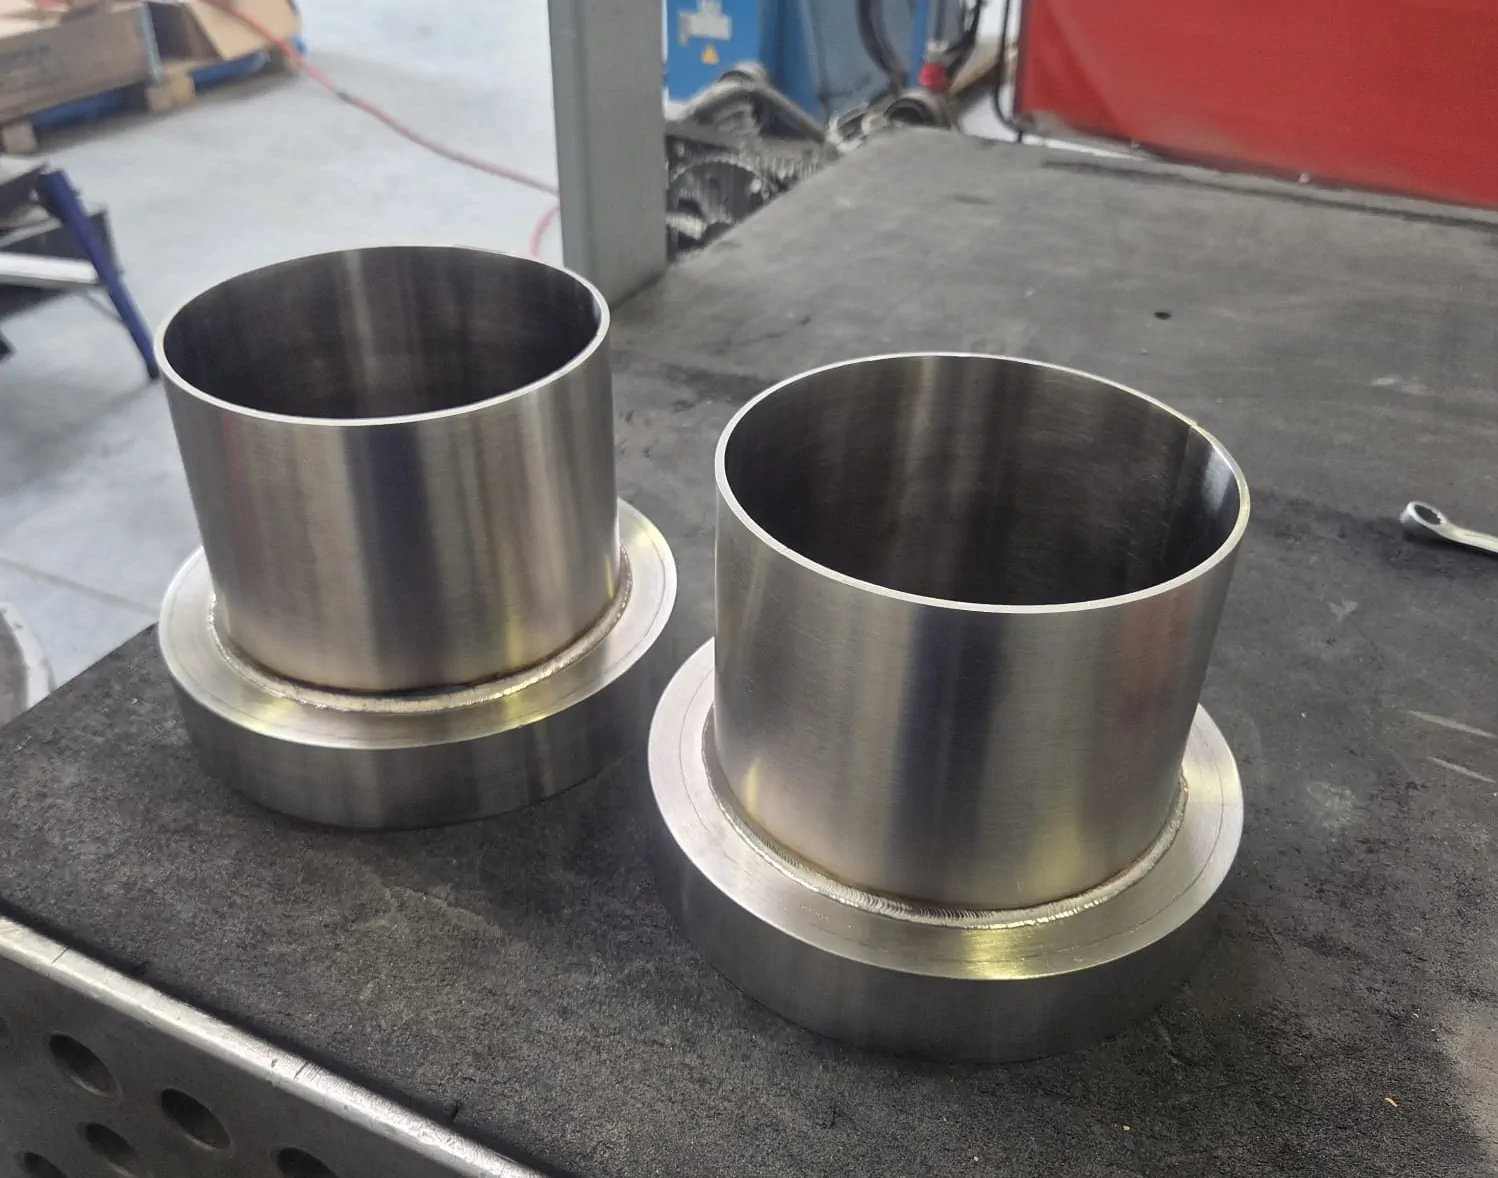
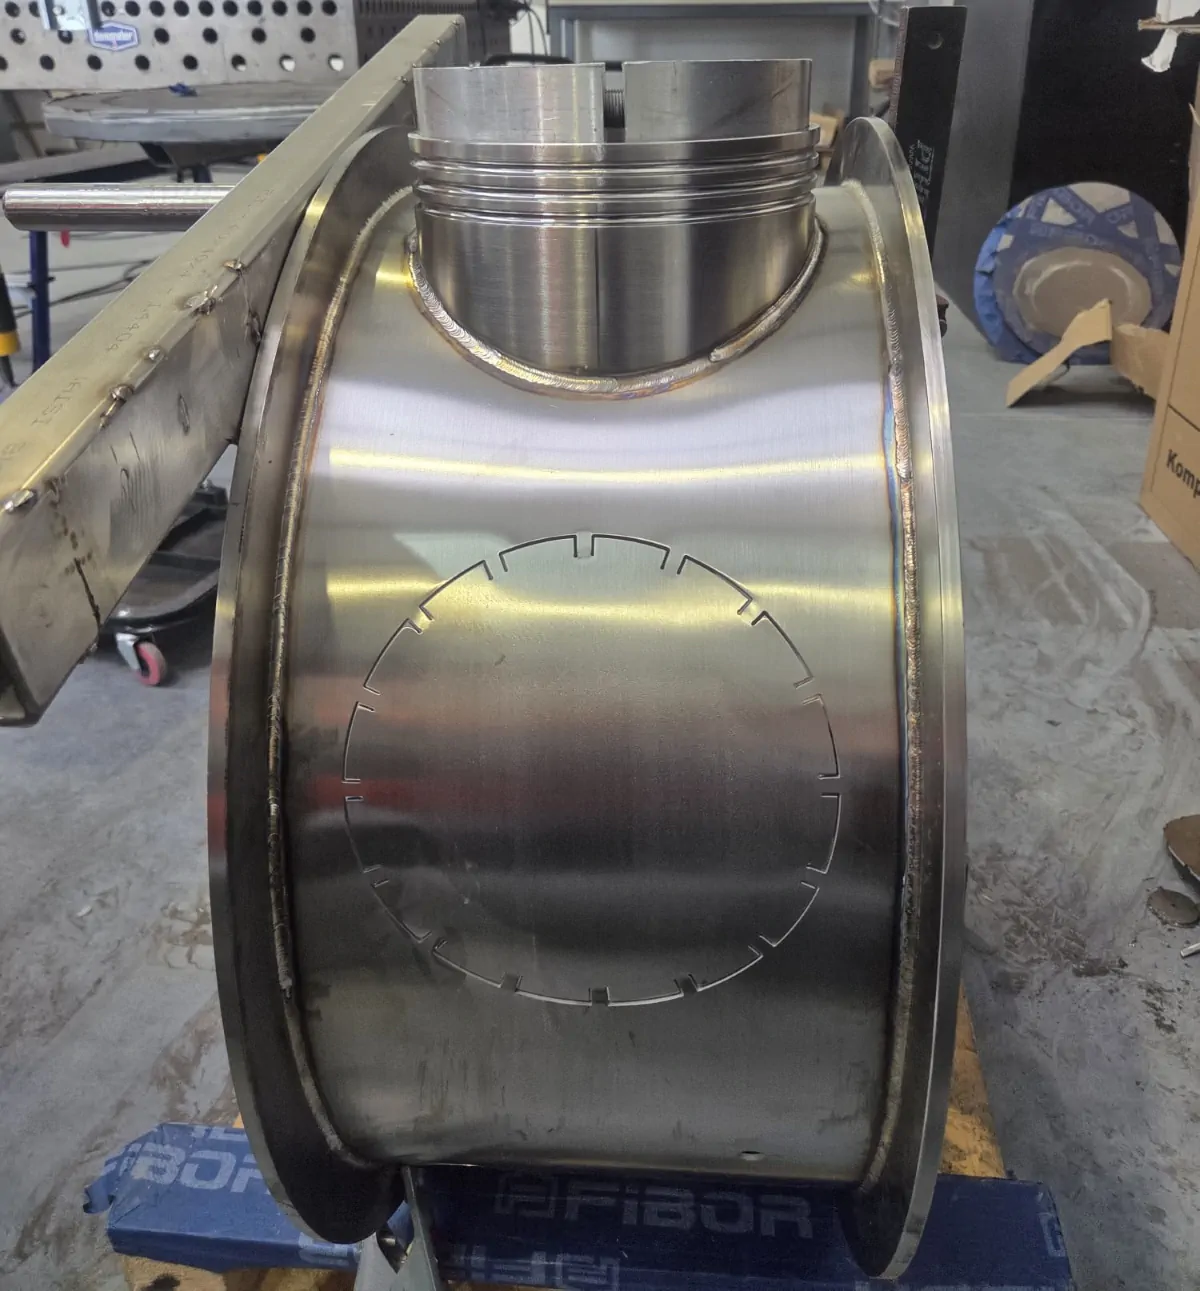
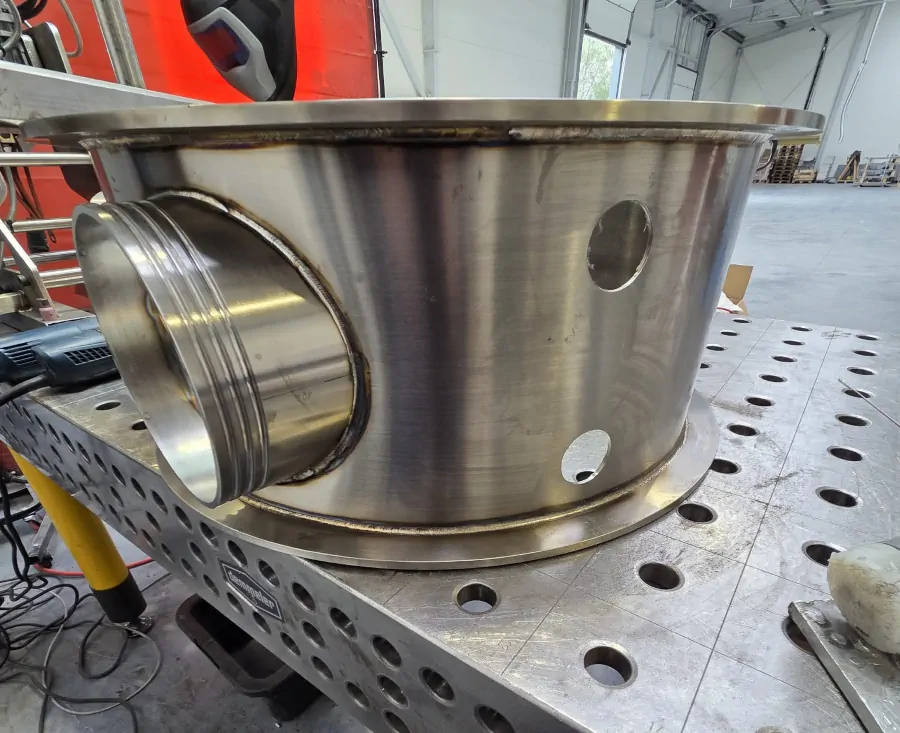
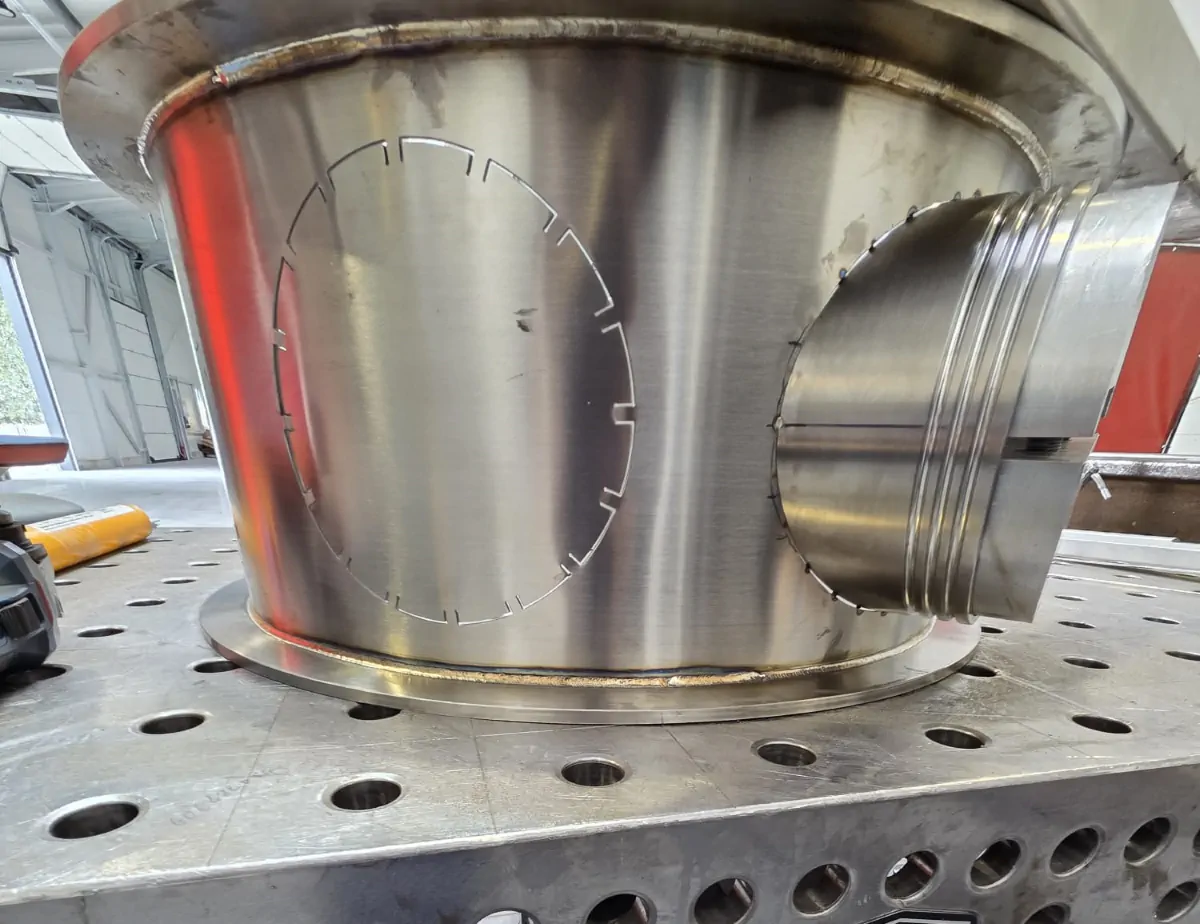
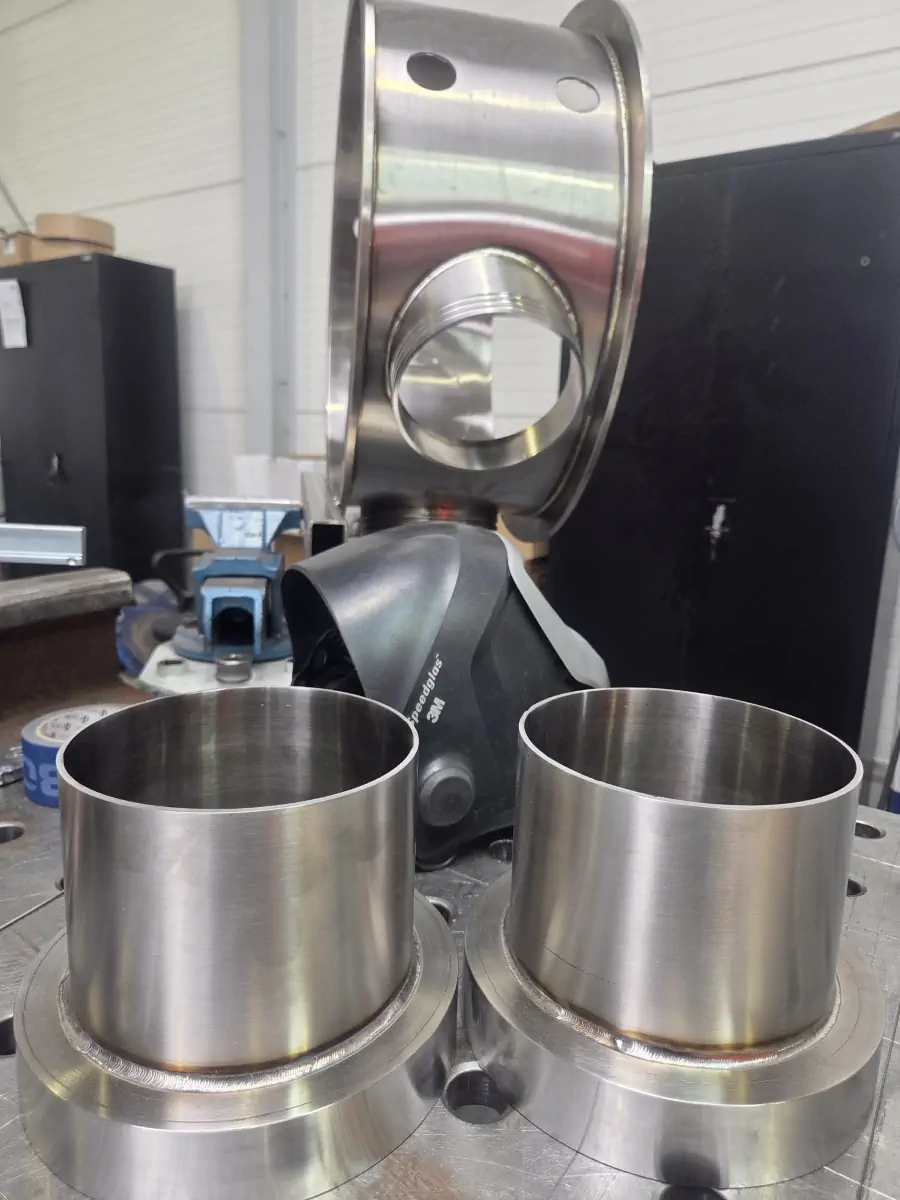
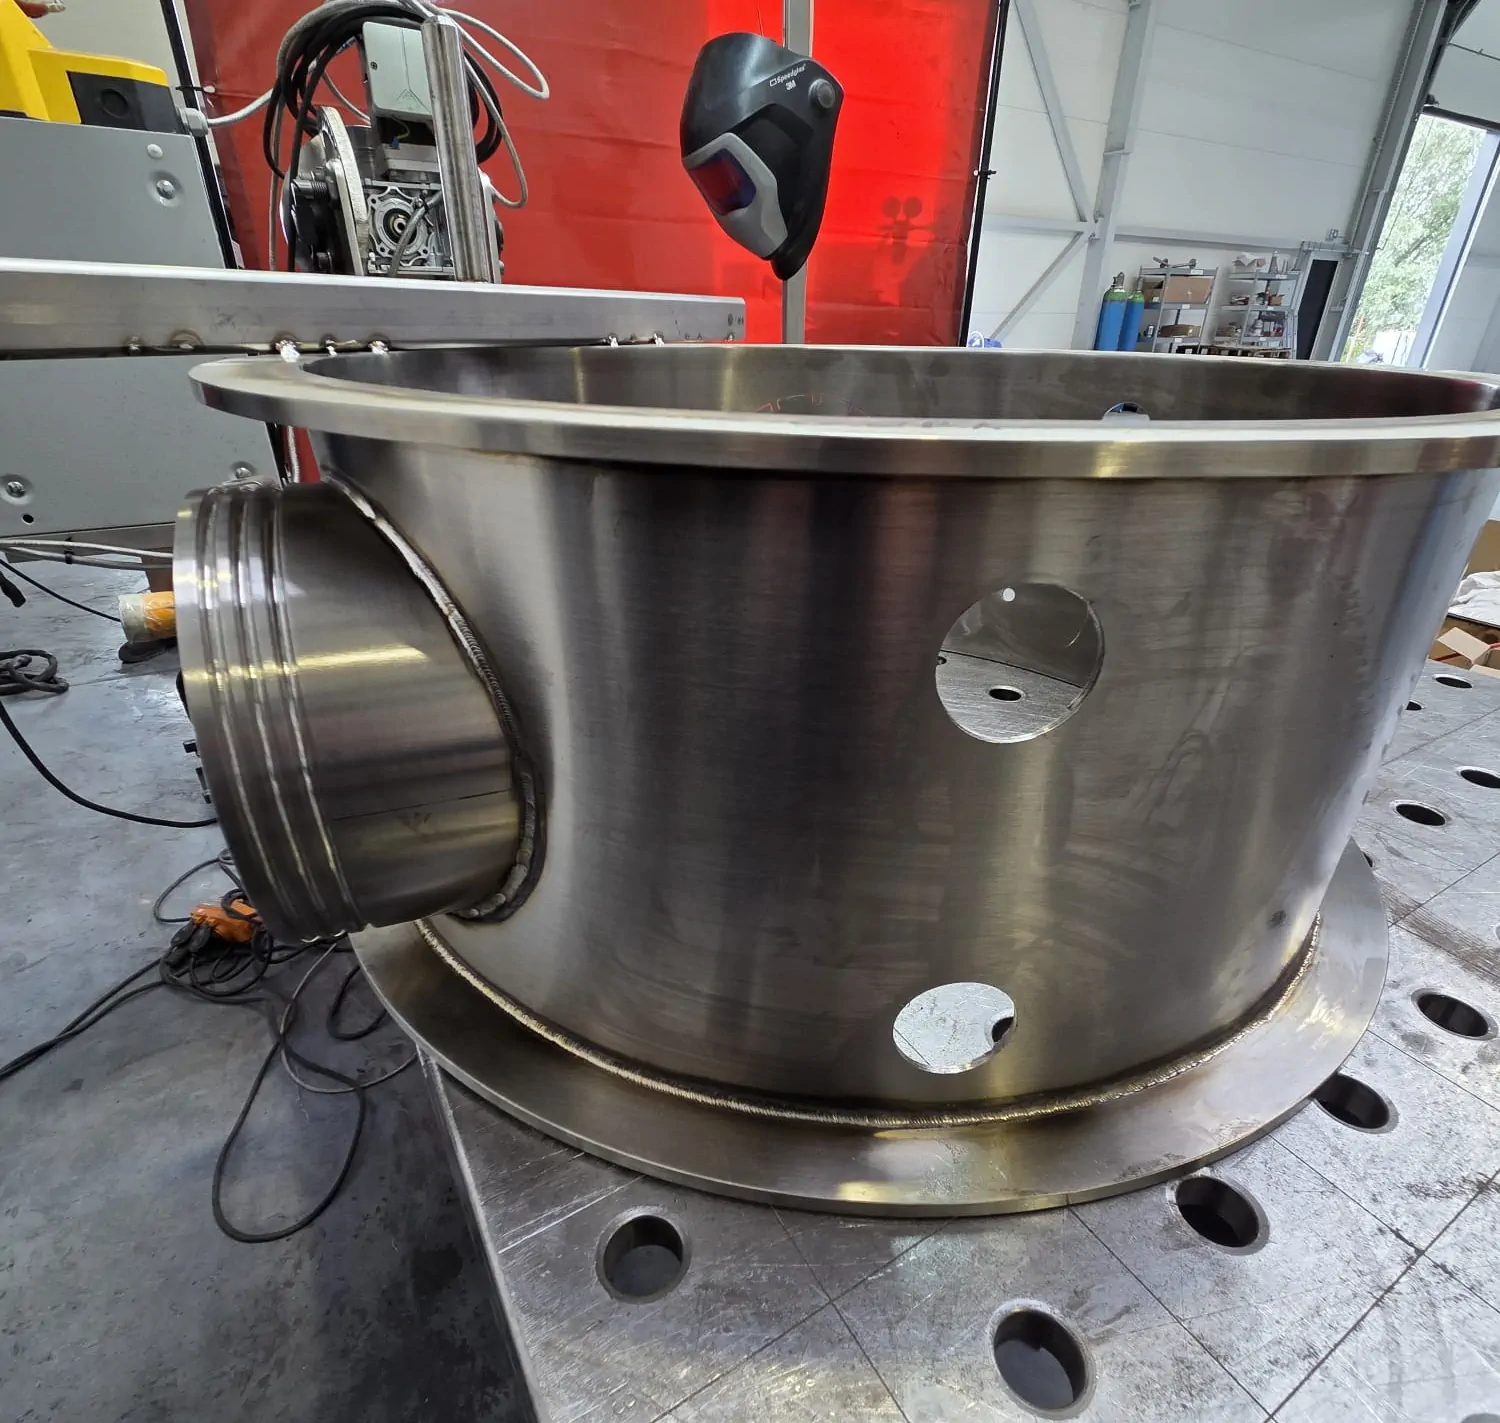
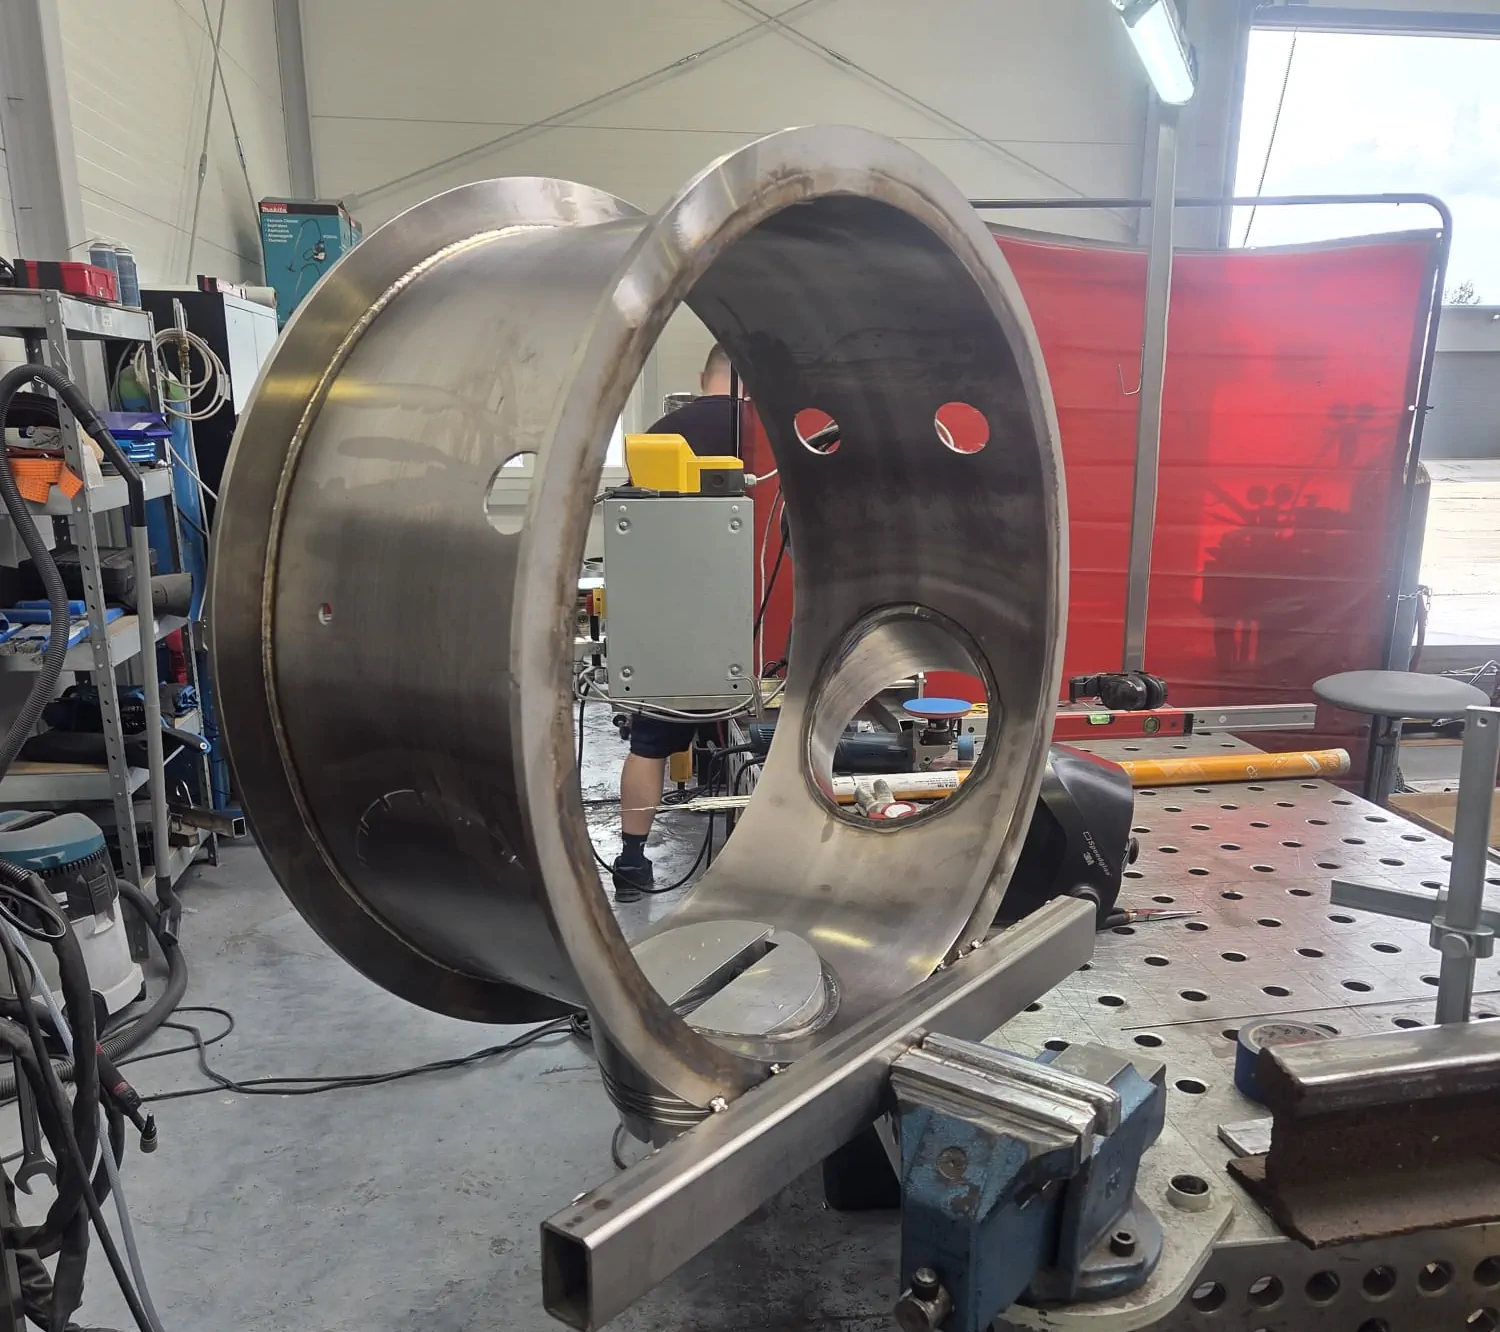
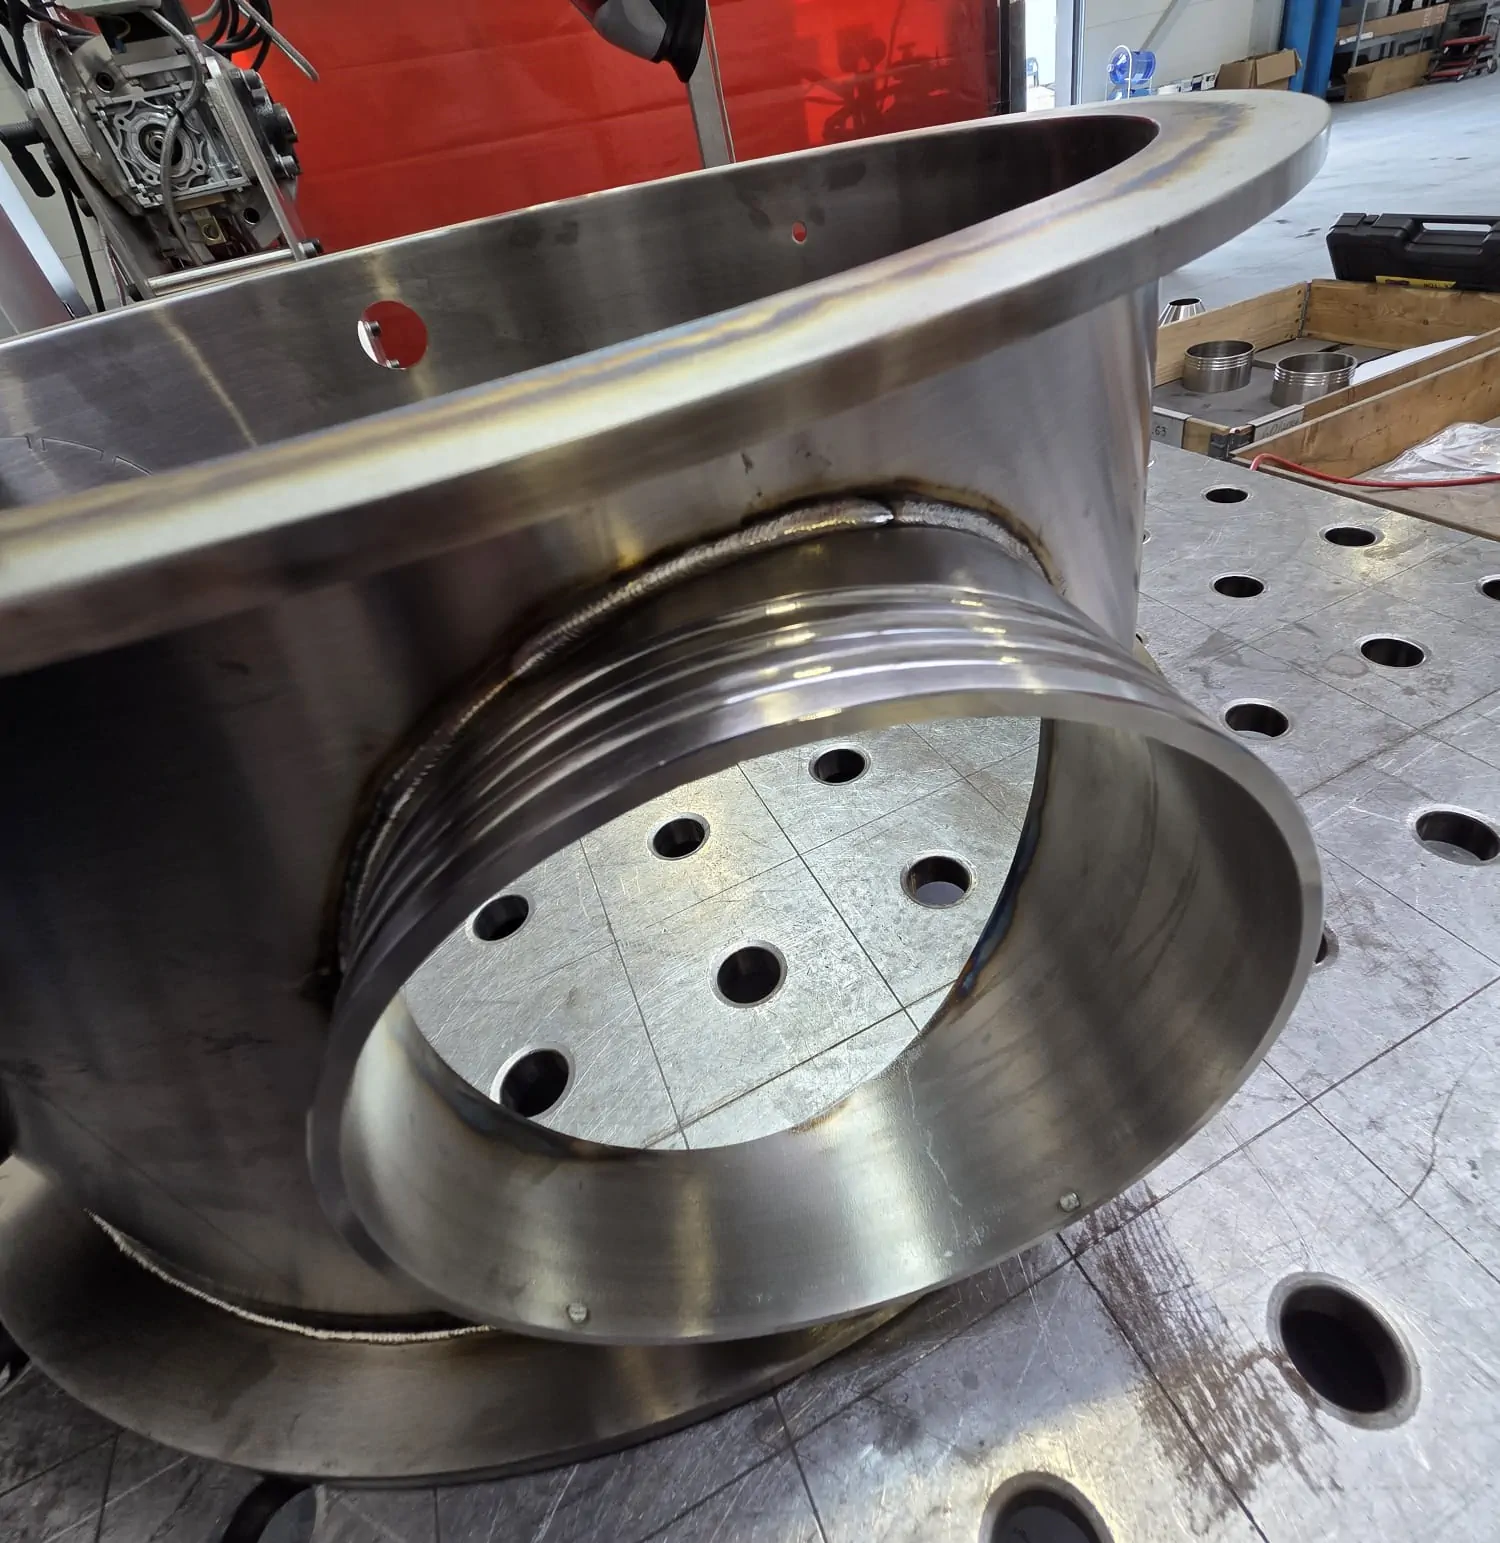
This project involves the fabrication of a precision DCS equipment body with a nominal diameter of DN600, designed for the installation of working gloves and nitrogen (N₂) connections. The structure is manufactured as a welded steel enclosure consisting of a cylindrical shell, flanges, process nozzles and reinforcing elements.
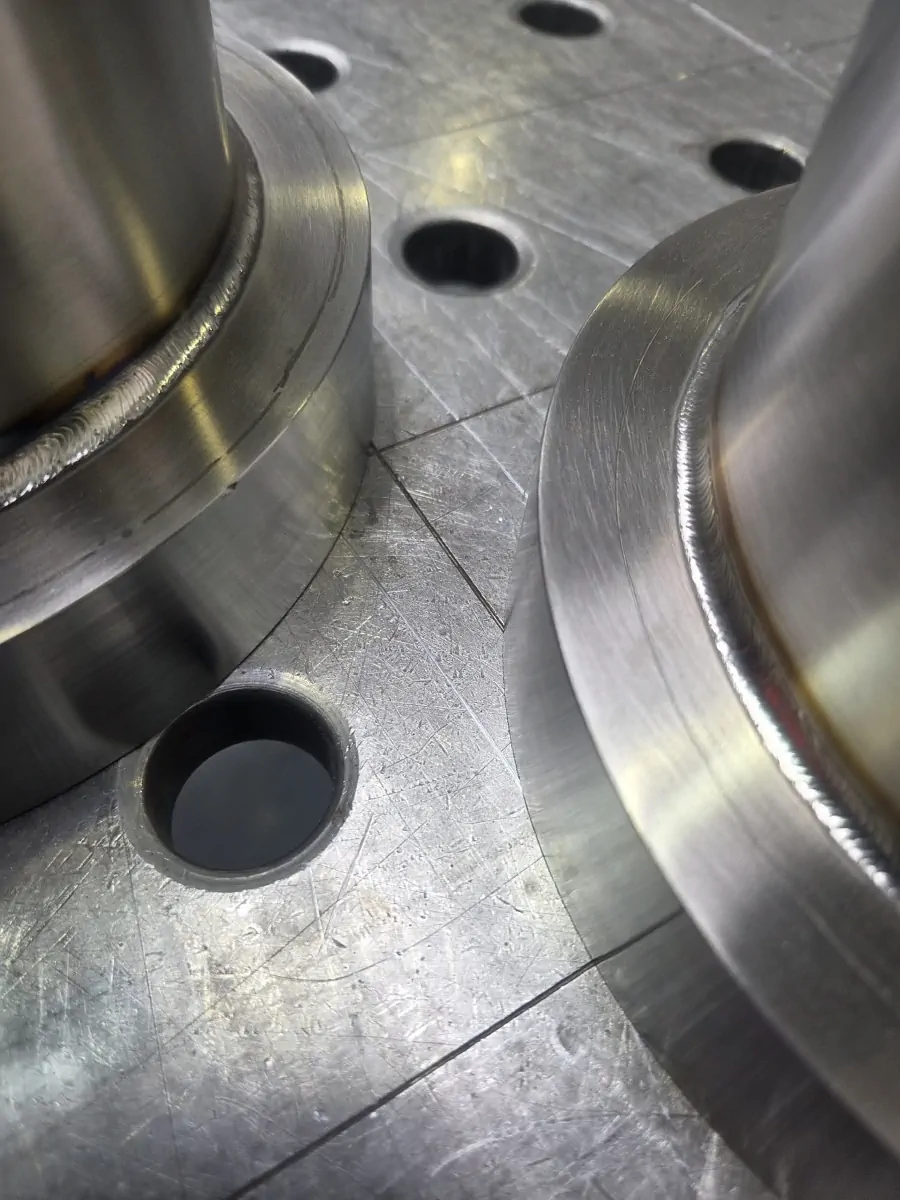
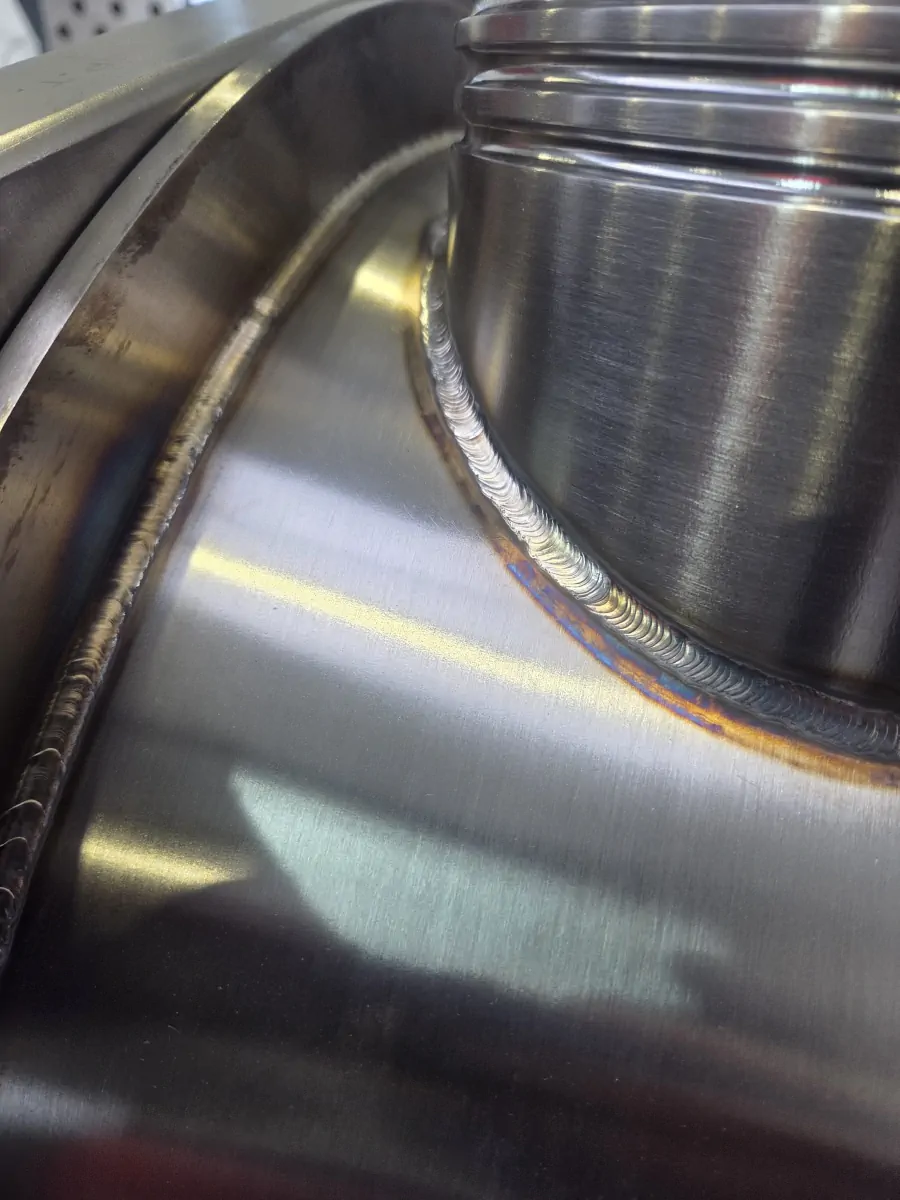
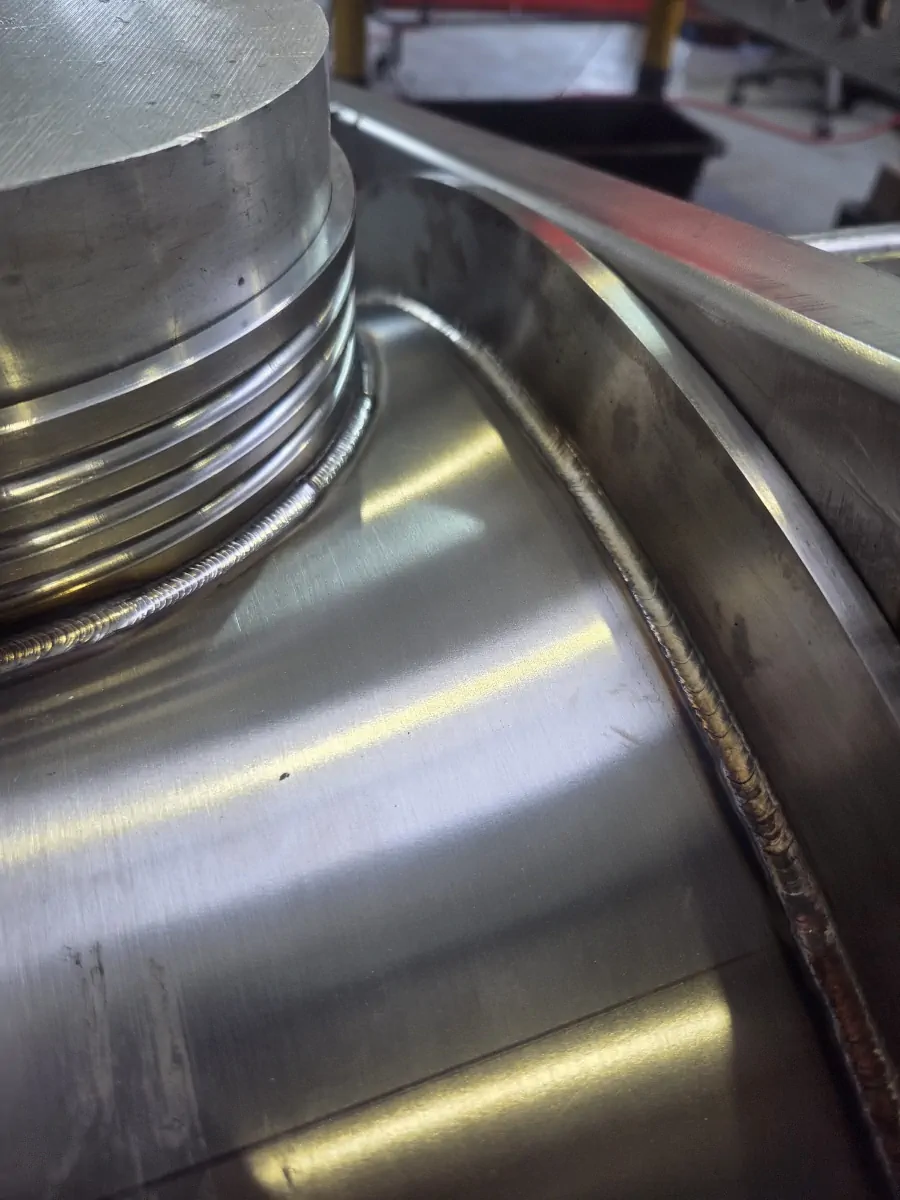
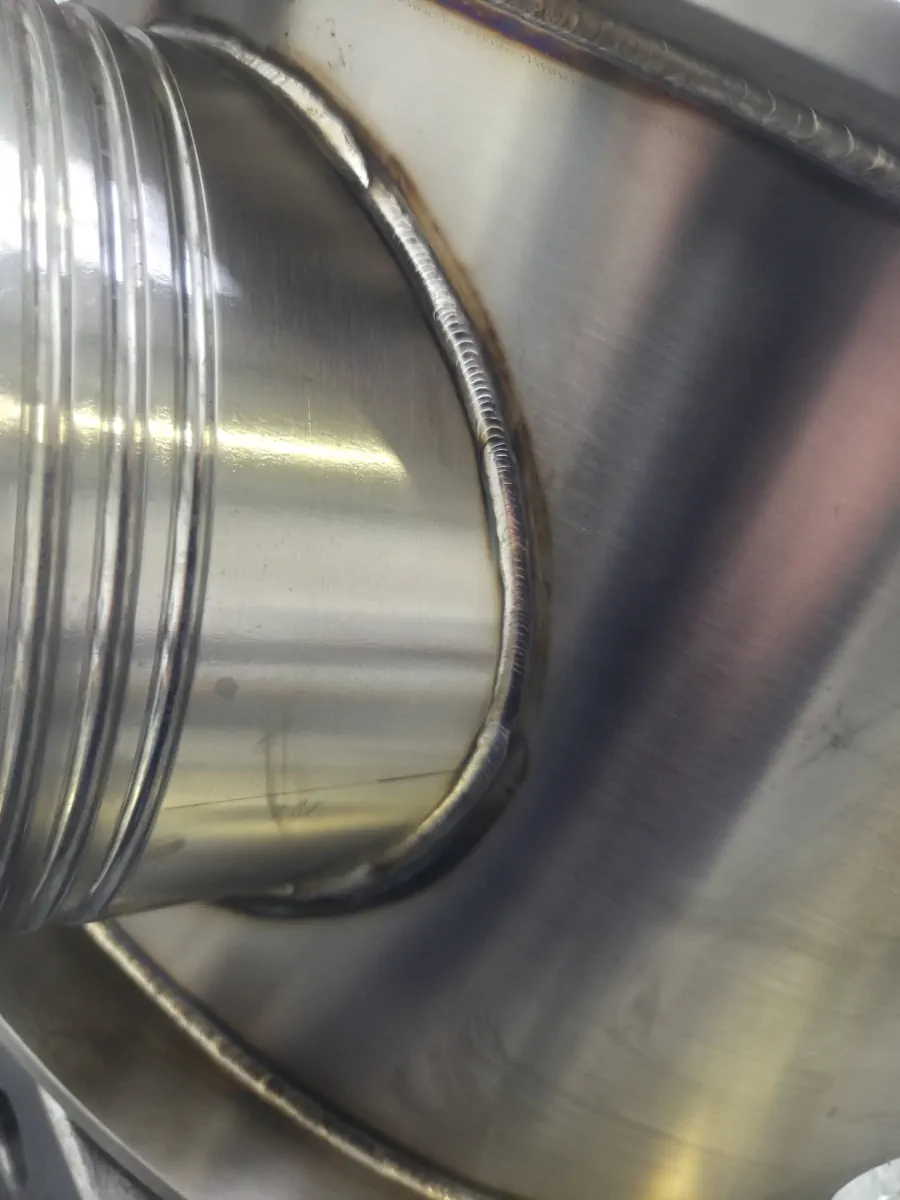
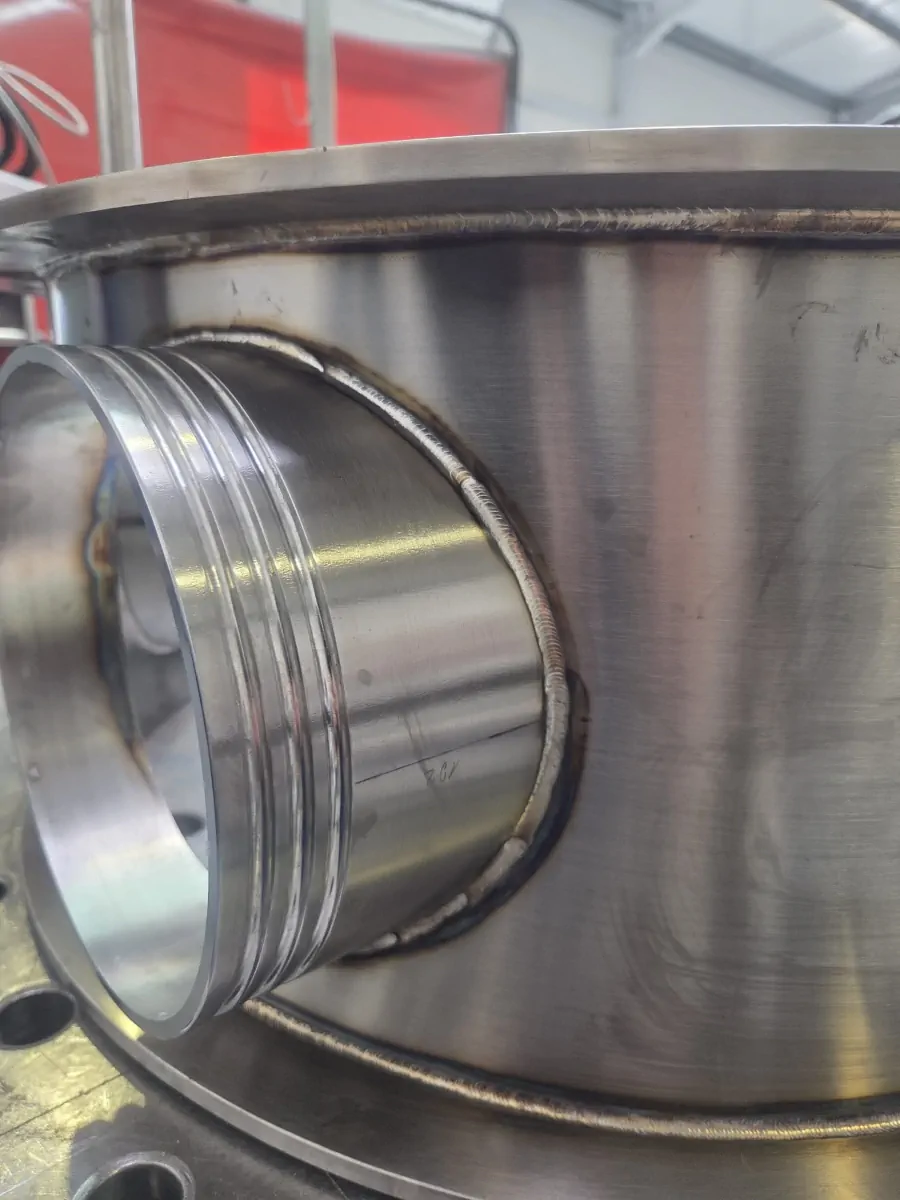
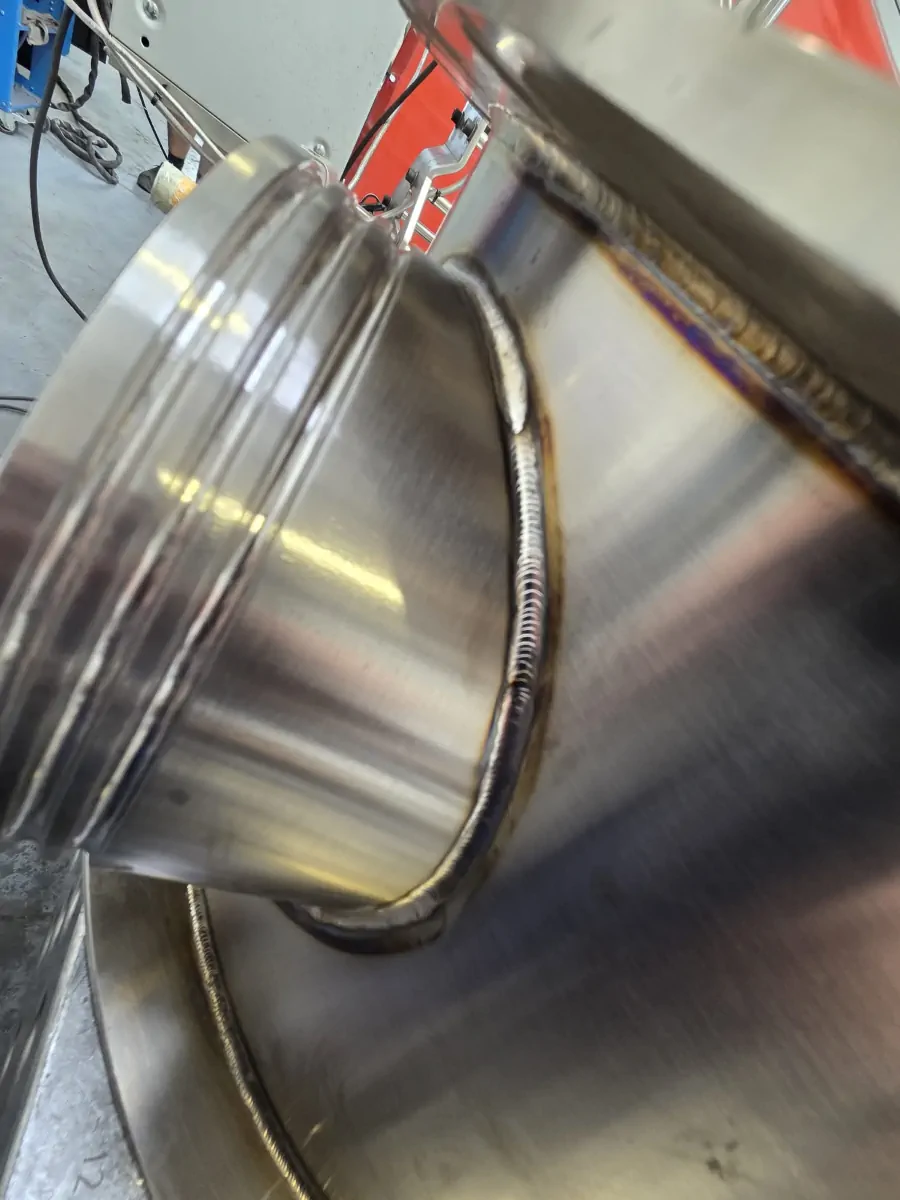
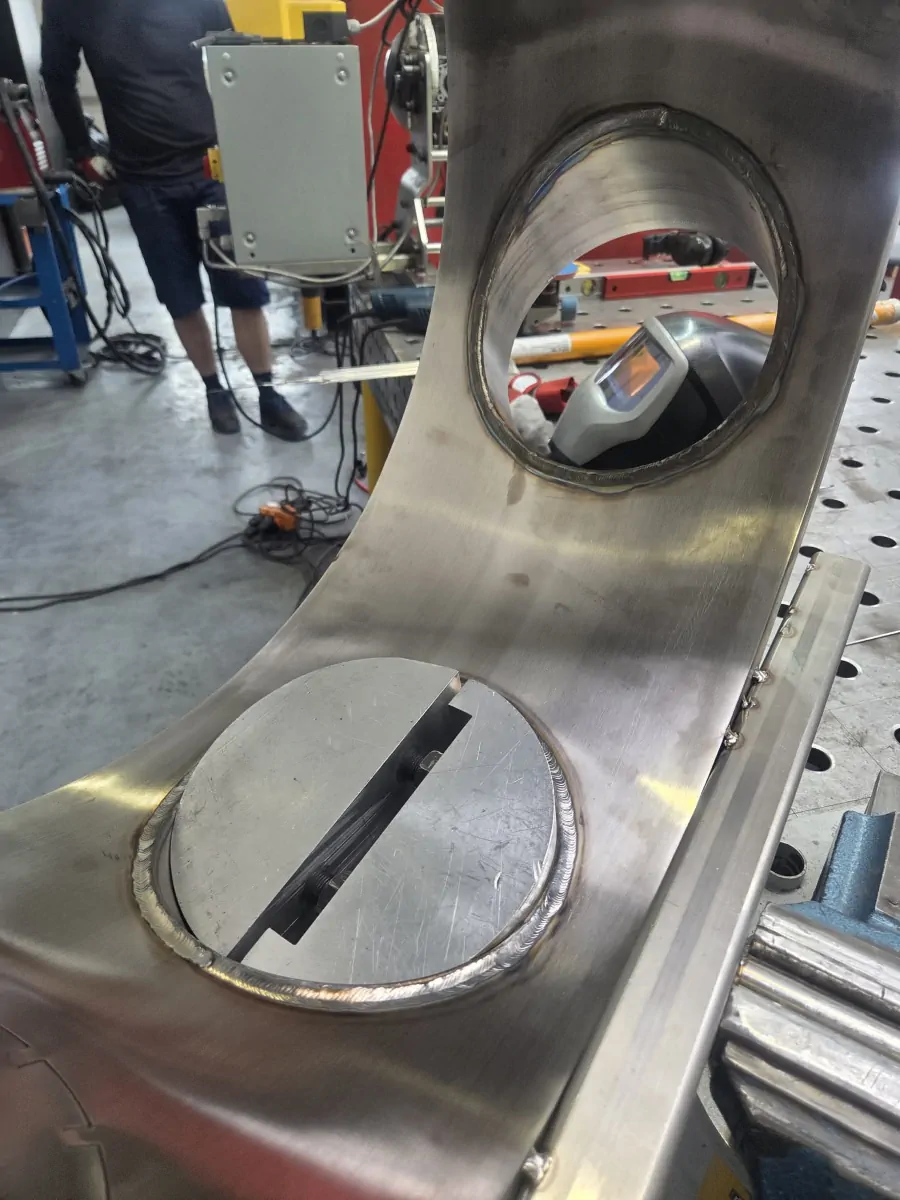
A key requirement of the project is to achieve a high-quality visual finish of the welds while maintaining very tight dimensional tolerances after welding. Particular attention is also paid to the flatness of the upper and lower rings, while the internal and external surfaces are finished to specified roughness values of Ra 0.5 µm internally and Ra 0.8 µm externally.
Construction
Size
DN600
Precision
Flatness control
upper and lower rings
Surface Finish
Ra 0.5 / Ra 0.8 µm
internal / external
Project objectives
The fabrication of the DCS body requires highly accurate preparation of individual components before welding begins. Due to the DN600 diameter and the combination of a cylindrical shell, flanges, process connections and reinforcing elements, precise fit-up and a carefully planned welding sequence are essential. This helps minimise welding distortion and maintain the required dimensions of the finished assembly.
Surface quality is equally important. The project requires clean, visually consistent welds, controlled flatness of both the top and bottom rings, and clearly defined surface-finish parameters. The inner surface is finished to Ra 0.5 µm, while the external surface is finished to Ra 0.8 µm, which requires careful control of both the welding process and subsequent surface treatment.
Technical specification
Details:
Project gallery